


 English
 русский
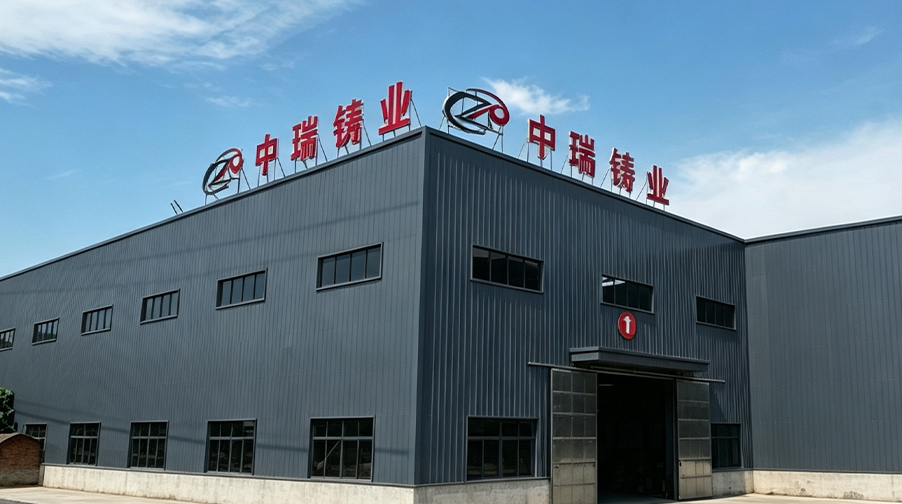
Anhui Ningguo Zhongrui Wear-Resistant Materials Co., Ltd. casts grinding cylpebs at our foundry in Ningguo City, Anhui Province, inside China's wear-resistant casting cluster. We pour high-chromium, medium-chromium and low-chromium alloy grades, form them on automatic iron-mould sand-coating and lost-foam lines, and heat treat every batch under our own roof. As a Grinding Cylpebs manufacturer, we size cylindrical media to the mill duty rather than to a catalogue default, for cement plants, mineral concentrators, thermal power stations and chemical processors.
Annual output of cast balls and castings is 60,000 tons, and a single trial charge runs through the same melting, pouring, quenching and annealing equipment as a scheduled make-up programme. That matters when a mill's wear rate and liner life are calculated against a known media grade.
Cylpebs in Our Casting Grinding Media Range
A grinding cylpeb is a cast cylinder, defined by diameter and length, charged alongside balls in the same mill. The flat ends and cylindrical body give line and face contact with the charge instead of the single point contact of a sphere, which makes cylindrical media a natural fit for fine-grinding chambers where size reduction depends on surface interaction rather than impact energy.
- Grades: high-chromium cast iron is our standard cylpeb material; medium-chromium and low-chromium alloy grades are cast for lower-abrasion feeds or a specified chemistry window.
- Forming routes: automatic iron-mould sand-coating lines and lost-foam precision casting, chosen by size, tolerance and order quantity.
- Heat treatment: temperature-controlled quenching followed by reheat treatment, with two automatic flipping annealing furnaces for stress relief.
- Size coverage: our small-dimension casting line produces cylindrical media and cast balls from 6 mm to 40 mm diameter, while the full cast media range spans Ф8 mm to Ф150 mm.
- Surface condition: every piece is inspected after pouring and then ground and polished before hardness verification.
Cylpebs and balls are not interchangeable inside a charge. A mill optimised for spheres needs its media mix, charge level and make-up rate reviewed before a cylindrical charge is introduced, and we work through that calculation with the customer during configuration.
Application Fit: Cement, Mining, Thermal Power and Chemical
Cylindrical media suit duties where fine grinding dominates and impact loading stays moderate. The table below maps the circuits we configure most often and the grade direction that normally follows from them.
| Application | Typical circuit | Why cylindrical media fit |
|---|---|---|
| Cement finish grinding | Second-chamber closed-circuit ball mill | Face and line contact lift the rate of fine size reduction; high-chromium grade resists abrasive clinker |
| Slag and blended cement | Dry closed circuit with separator | Cylindrical media keep contact with a fine, dry, free-flowing charge |
| Concentrator re-grind | Secondary or tertiary grinding stage, fine feed | Smaller make-up sizes limit over-grinding; grade follows ore abrasiveness |
| Thermal power pulverising | Dry mill with mixed charge | Consistent geometry supports steady output and predictable make-up tonnage |
| Chemical and mineral filler | Batch or continuous dry mill | Grade selected against corrosion risk and product contamination limits |
The Wider Grinding Media and Wear Parts We Cast
Cylpebs sit inside a broader cast wear programme. The same alloy bank and heat treatment line produce the media, liners and crushing parts that surround them, which keeps grade and delivery planning on one schedule.
| Product | Form and material | Where it fits |
|---|---|---|
| Grinding Cylpebs | Cylindrical cast media in high, medium and low chromium alloy | Fine-grinding chambers, dry grinding, re-grind circuits |
| Grinding Ball | Spherical cast media from small-dimension up to 150 mm | Primary and secondary grinding, high-impact duty |
| Grinding Rods | Cast rod media, alloy matched to the duty | Coarse grinding where low over-grinding is required |
| Casting Ball Mill Liner | High-chromium, high-manganese and medium-chromium alloy liners | Shell and end liners, planned with the grinding charge |
| Crusher Wear Casting Parts | Chromium hammers, jaw plates, crusher liners | Upstream crushing ahead of the grinding circuit |
Material, Geometry and Specification Variables
Every cylpeb order is fixed on three axes: chemistry, geometry and heat treatment. The table shows what we control on our side and what we need from the plant to lock the specification.
| Variable | What we control | What we need from you |
|---|---|---|
| Chemistry and grade | High, medium or low chromium cast iron with chromium, carbon, manganese and silicon balanced to the grade | Feed material, abrasiveness, wet or dry operation, any corrosion risk |
| Cylpeb size | Diameter and length within the small-dimension casting range, held to drawing or agreed tolerance | Mill diameter and chamber length, current media mix, target make-up size |
| Hardness | Quench and reheat parameters set to the grade, verified on our hardness tester | Required hardness window and where it is checked |
| Impact and breakage | Grade and heat treatment matched to mill impact severity | Mill speed, charge drop conditions, breakage history with current media |
| Surface and internal soundness | Visual acceptance for cracks, slag inclusions, pores, sand holes, shrinkage cavities and cold shuts, then polishing | Acceptance criteria and inspection scope |
| Packing and marking | Format, batch separation and labelling agreed at order confirmation | Shipment tonnage, handling equipment, labelling language |
Melting, Pouring and Heat Treatment Control
Three VIP-1800 series melting furnaces feed the cylpeb line, and each heat is tracked from raw material to finished product across our casting ball workshop, casting workshop, white mould cutting workshop, heat treatment workshop and finished product workshop.
- Chemical analysis: a cabinet-type PRO spectrometer and carbon-sulfur analyzer read over a dozen elements within about a minute. Analysis runs before and after melting, and any deviation is corrected before the heat is released for pouring.
- Pouring: far-infrared temperature measurement sets the pour, and the automatic iron-mould sand-coating lines pour at constant temperature to keep geometry and solidification consistent.
- Heat treatment: an automatic quenching plus reheat treatment line and two automatic flipping annealing furnaces set hardness and relieve casting stress.
- Inspection: first visual inspection rejects surface defects, and passing pieces are ground and polished before hardness verification in the physical property testing room.
Quality Assurance, Certification and Acceptance
Because each heat is analysed before and after melting, the composition behind a delivered lot traces back to its batch. Hardness, surface condition and dimensional checks are the acceptance points we agree with the customer before shipment.
- ISO9001 quality, ISO14001 environmental and ISO45001 occupational health and safety management certification, with Safety Production Standardization certificates held by the company.
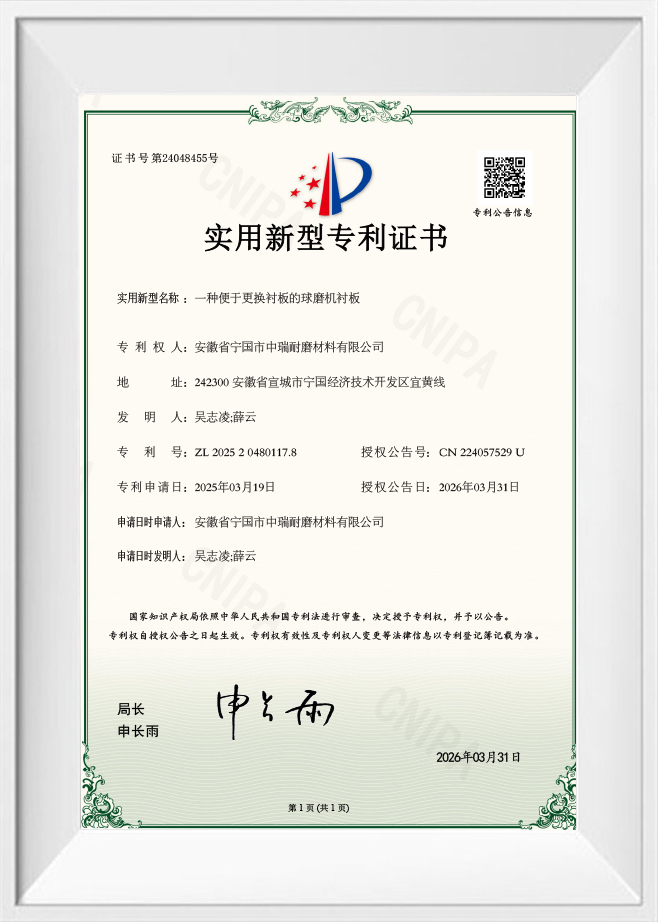
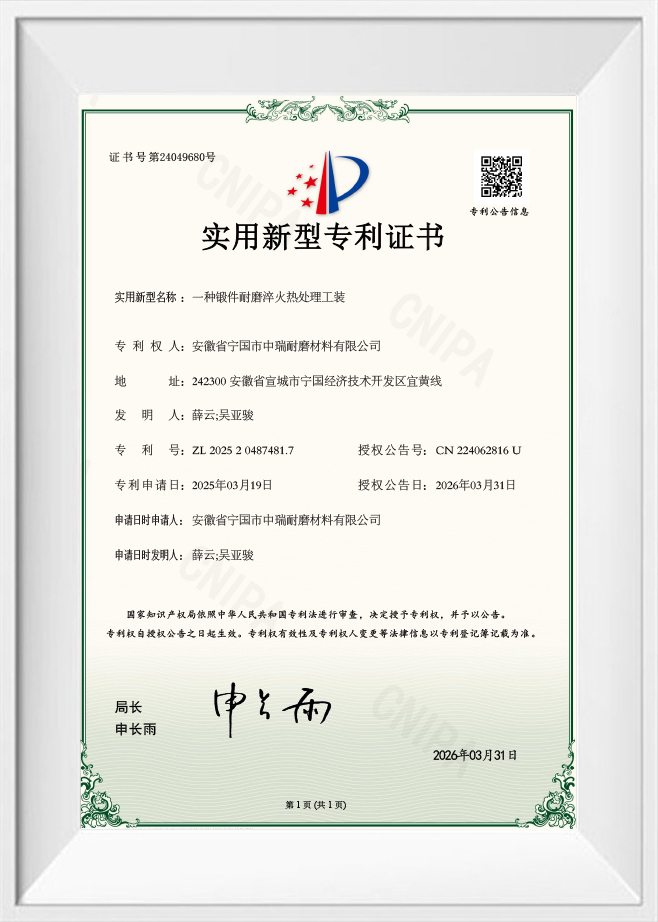
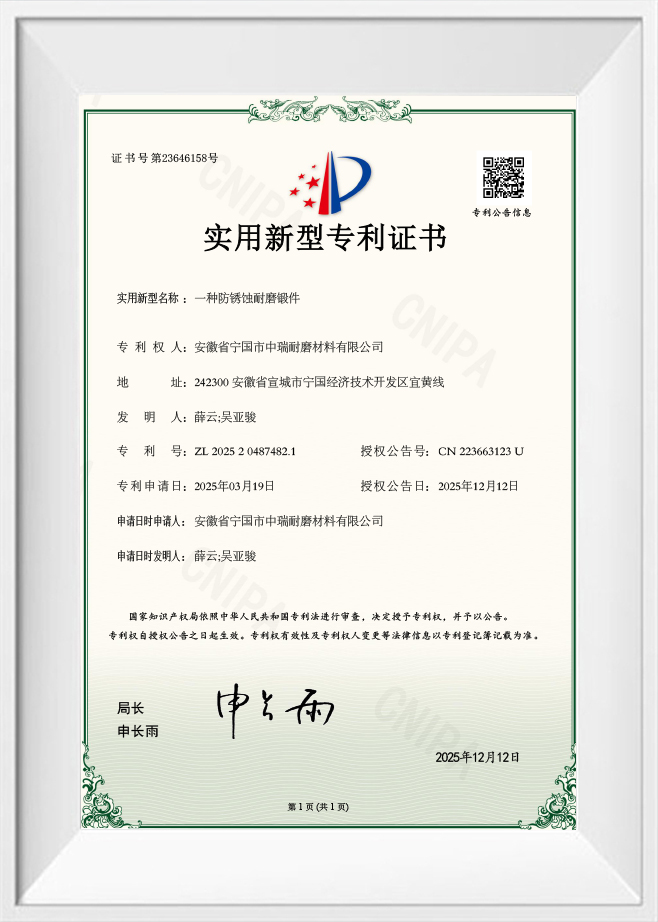
- Utility model patent certificates covering casting process equipment are part of the company's registered achievements.
- Acceptance scope — hardness verification, visual casting quality and dimensional checks — is confirmed per order so that the criteria used at the foundry match those used at the receiving plant.
Information We Use to Configure Your Solution
- Mill type, diameter, chamber length, rotational speed and whether the circuit is open or closed.
- Feed material and its abrasiveness — clinker, slag, ore type, coal or mineral filler — with feed and product size.
- Current charge: media mix and top size, charge level, liner profile, and historical wear or breakage data.
- Target performance: make-up rate per ton ground, expected wear life, and the breakage limit the mill can tolerate.
- Order pattern: tonnage per shipment, delivery schedule, packing format and labelling requirements.
- Documentation and compliance expectations for the receiving site.
With these inputs we return a grade recommendation, a diameter and length combination, and a quoted tonnage that matches the make-up rate the mill is already running. Enquiries received on working days are answered within 12 hours.
Packing, Delivery Scope and Ongoing Supply
Packing format is agreed at order confirmation and matched to the handling equipment at the receiving plant, with batches kept separate and labelled so the charge can go straight into the mill without re-sorting. Heavier shipments are planned around the customer's unloading method rather than a fixed standard package.
Because grinding media and mill liners are cast in the same plant, replacement charges and liner sets can be scheduled together. Wear parts for the surrounding circuit — crusher hammers, jaw plates and crusher liners — follow the same alloy discipline, so a plant replacing media and liners on one maintenance window deals with one supply programme.
Frequently Asked Questions
What is the difference between a grinding cylpeb and a grinding ball?
A cylpeb is a cast cylinder, a ball is a sphere. The cylinder presents line and face contact to the charge; the sphere contacts at a point. That difference makes cylpebs better suited to fine-grinding chambers, while balls carry more impact energy in coarse and primary grinding stages.
Which alloy grades do you cast for grinding cylpebs?
High-chromium cast iron is our standard grade. We also pour medium-chromium and low-chromium alloy grades where the feed is less abrasive or where the mill environment calls for a different chemistry window. The grade recommendation follows the abrasiveness of the feed, the wet or dry condition of the circuit and the mill's impact severity.
What cylpeb sizes can we order?
Our small-dimension casting line covers cylindrical media and cast balls from 6 mm to 40 mm diameter, and the cast media range overall spans Ф8 mm to Ф150 mm. Length is fixed with the diameter at order stage, so the cylinder geometry matches the chamber and the make-up size the mill requires.
How is quality controlled before shipment?
Molten iron is analysed before and after melting with a cabinet-type PRO spectrometer and carbon-sulfur analyzer, poured at constant temperature measured by far-infrared equipment, then quenched, reheated and annealed. Every piece passes visual inspection for cracks, slag inclusions, pores, sand holes, shrinkage cavities and cold shuts, and is polished before hardness verification.
What do you need from us to quote a cylpeb charge?
Mill type and dimensions, chamber, feed material and product size, current media mix and charge level, target make-up rate, shipment tonnage and packing preference. With those details we return a grade and size recommendation together with a quoted tonnage.
Can grinding cylpebs and mill liners be ordered together?
Yes. Cylpebs, cast grinding balls, grinding rods and ball mill liners are produced in the same foundry, so grade selection and delivery scheduling can be planned as one programme for a single maintenance window.



