


 English
 русский
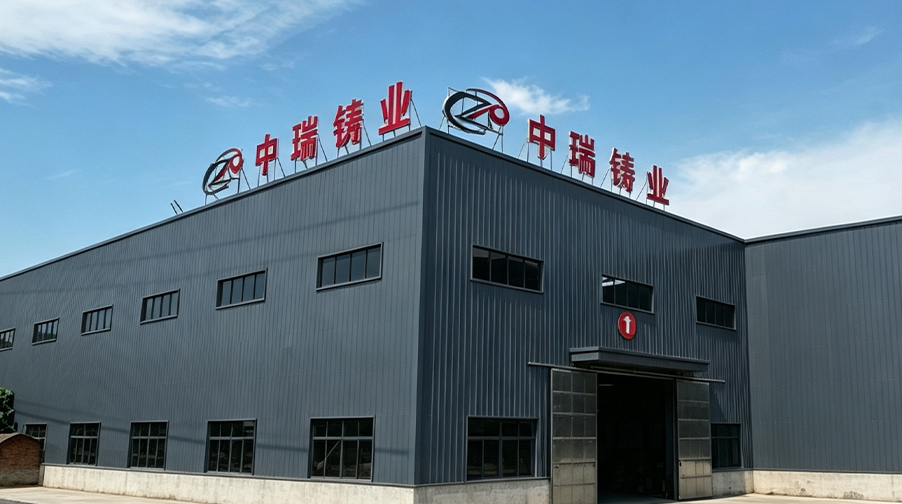
Anhui Ningguo Zhongrui Wear-Resistant Materials Co., Ltd. casts wear parts for grinding and crushing circuits at our foundry in Ningguo City, Anhui Province, China. Our Casting SAG Mill Liner manufacturer range covers the shell, head, grate and pulp-lifter castings used in semi-autogenous grinding mills, poured in high-chromium cast iron, medium-chromium alloy steel, high manganese steel and bimetallic composite grades.
Liners are produced on our lost foam vacuum casting line and on automatic iron-mold sand coating and shell molding lines, then finished with temperature-controlled quenching, re-heat treatment and annealing. Each set is matched to a mill diameter, charge profile, ore condition and discharge arrangement rather than issued as a single universal grade.
What we cast for SAG circuits
- Shell liner plates and lifter bars, including rib, wave, step and smooth profile variants
- Feed-end and discharge-end head liners in heavier sections
- Grate liners, pulp lifters and end-cap protection castings
- Trunnion and shell-protection components
- Rubber and Mn-Cr alloy cast composite liner assemblies
Our Position in the Casting Mill Liner Family
The Casting Mill Liner family covers horizontal mills: SAG and AG shell liners, Casting Ball Mill Liner plates and vertical mill liners. SAG work sits at the heavy end of that family: larger castings, thicker sections, higher direct impact from the falling charge and a wider spread between abrasion-dominated and impact-dominated zones.
We pour liners alongside high-chromium, medium-chromium and low-chromium cast balls, cast sections, crusher guards and hammers, with an annual output of 60,000 tons of cast balls and castings. Heavy castings are produced up to 5000 × 5000 × 1000 mm within a 1500 kg single-piece envelope, and thick compact castings to 1500 × 1500 × 1200 mm at up to 3000 kg per piece. That range lets us quote a full liner set rather than shell plates alone.
Liner Types and Where Each One Fits
- Shell plates and lifter bars form the lifting profile along the barrel. Profile selection controls charge trajectory, toe position and the balance between tumbling and direct impact.
- Feed-end head liners face the steepest impact angle in the mill and are normally cast in work-hardening manganese steel or a composite arrangement.
- Discharge grate liners and pulp lifters govern open area, slot wear and pulp return; slot geometry is cast or machined to the mill's throughput target.
- Trunnion and end-cap castings protect sealing and support surfaces where access for replacement is difficult.
- Composite assemblies such as the rubber and Mn-Cr alloy cast composite liner for SAG mill reduce liner mass in zones where impact energy is moderate.
Material Selection by Duty Zone
| Grade family | Typical SAG position | Controlling property |
|---|---|---|
| High-chromium cast iron | Shell plates in abrasion-dominated zones | Abrasion resistance, hardness retention |
| Medium-chromium alloy steel | Shell and end sections with mixed impact and abrasion | Toughness with moderate wear rate |
| High manganese steel (Mn13Cr2, Mn18Cr2 class) | Feed-end liners, high-impact lifter faces | Work hardening, crack resistance |
| Bimetallic and composite castings | Grate, pulp lifter and transition areas | Hard wear face on a ductile backing |
| Rubber and Mn-Cr composite | Lower-impact shell and end zones | Mass reduction, noise, fine-particle wear |
Grade selection follows the wear pattern we see in the mill, not a catalogue default. Where a shell has shown cracking at the lifter fillet or spalling across the plate face, the alloy and heat treatment route are adjusted together, because impact toughness and hardness have to be balanced at the same working point.
Profile, Geometry and Fastening Configuration
Profiles are set from the mill's speed, charge level and target throughput. We cast lifter height, face angle, top width, plate thickness and taper to the duty required, and reproduce existing OEM geometries from drawings, worn samples or a laser scan of the shell.
- Bolt-hole pitch, countersink angle and bolt circle diameter are verified against the mill drawing before pattern work.
- Chord length, curvature radius and plate-to-plate gaps are checked so the set closes correctly around the barrel.
- Lifter bar spacing and row count are configured for the required charge trajectory and power draw.
- Backing compound grooves, rubber backing and sealing washers are included where the fastening system requires them.
Melting, Pouring and Heat Treatment
Our foundry runs 3 sets of VIP-1800 series melting furnaces, 2 fully automatic iron-mold sand coating lines, 4 mechanical-arm shell molding machines, 1 fully automatic lost foam mold production line, 1 automatic quenching and re-heat treatment line and 2 automatic flipping annealing furnaces.
Molten iron is analysed with a cabinet-type PRO spectrometer and a carbon-sulfur analyzer before and after melting; composition is corrected before pouring. Far-infrared instruments measure molten steel temperature at constant-temperature pouring. Quenching and annealing are temperature-controlled, which stabilises the metallographic structure through the full section of a thick liner casting.
Quality Control and Acceptance Evidence
- Chemical composition verified per heat before and after melting
- Hardness testing in the physical property testing room
- Visual and dimensional inspection of each casting for cracks, slag inclusions, pores, sand holes, shrinkage cavities and cold shuts
- Grinding and polishing of accepted semi-finished castings
- Heat-number traceability from pattern batch through to packing list
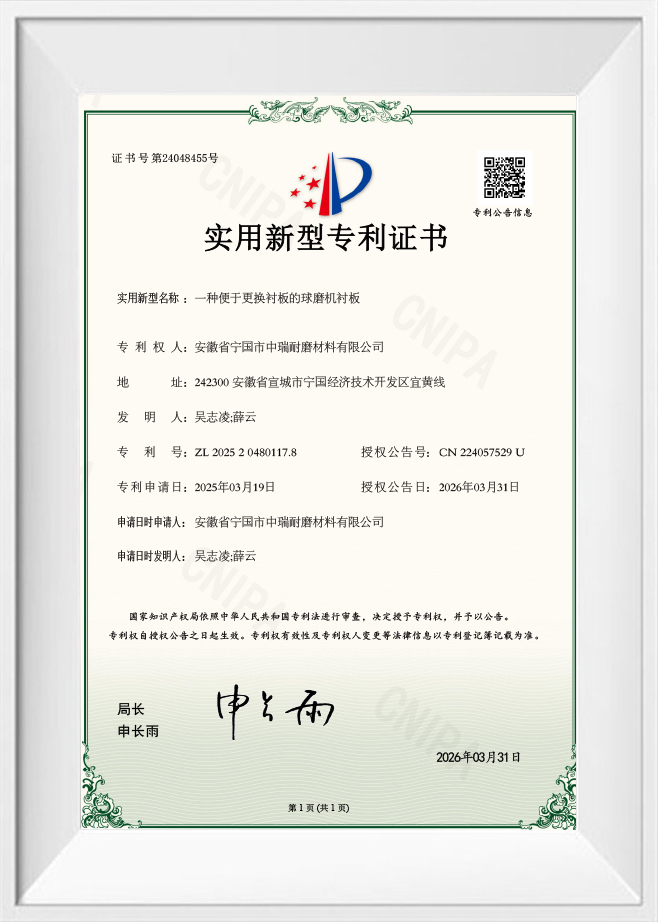
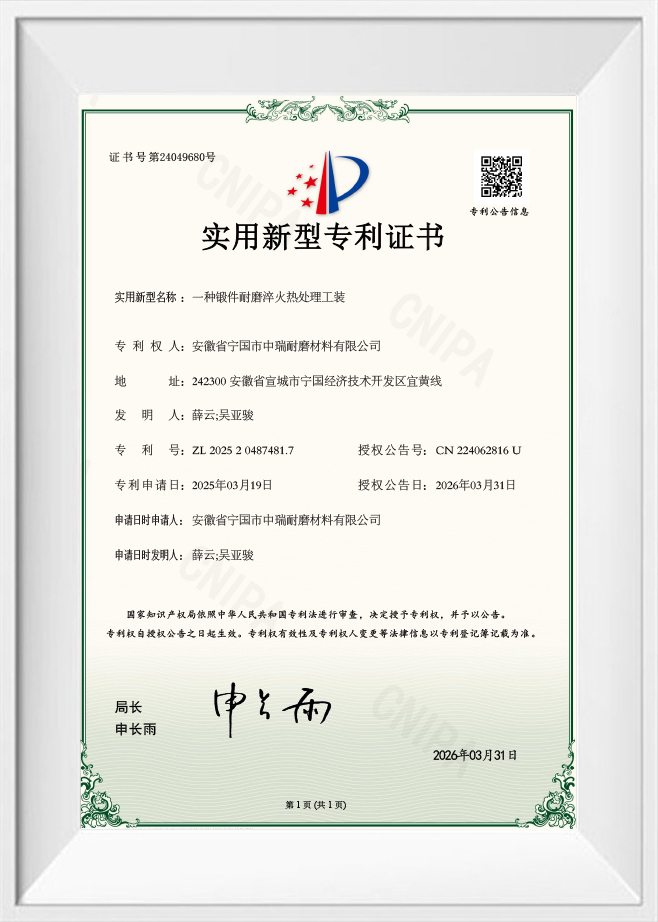
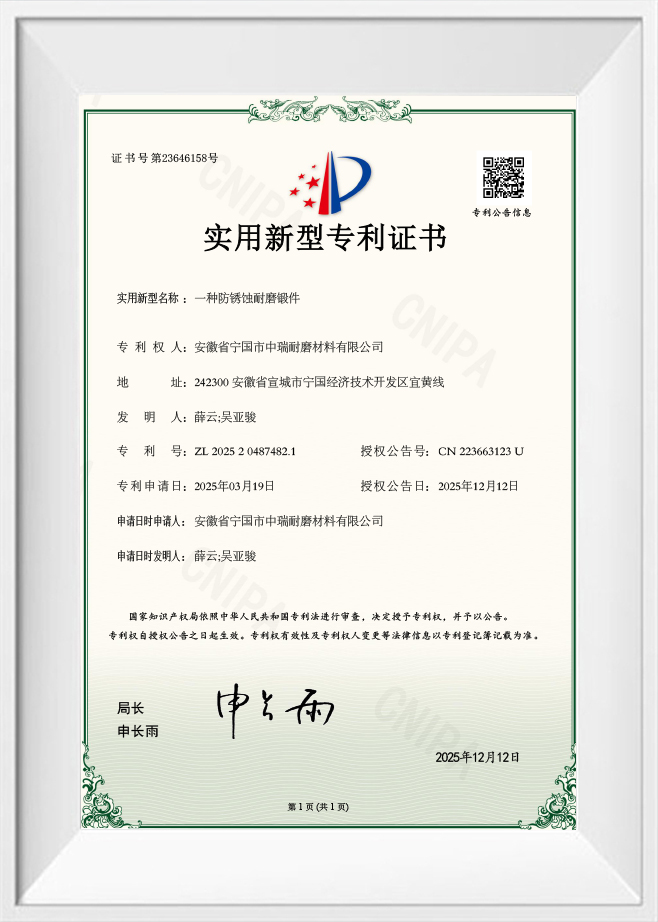
Our management systems are certified to ISO9001, ISO14001 and ISO45001, and we hold Safety Production Standardization certification together with utility model patents covering production equipment and processes. Mill test certificates, hardness reports and dimensional records are issued with the shipment.
Installation, Commissioning and Maintenance Support
Liner sets ship with a position-marked layout drawing so plates and lifters are installed in the intended order. We confirm bolt grade, torque values, seal arrangement and backing-compound specification against the mill's fastening system, and support the change-out sequence for shell, head, grate and pulp lifter sections.
During the first running period, bolt re-torque, plate seating and discharge slot opening are the checks that matter most. For ongoing operation we work from thickness measurements and inspection records to plan liner rotation, staged replacement and spare-part stocking, and replacement castings are produced to the same pattern and heat-treatment route so that wear data stays comparable across campaigns.
Information We Use to Configure Your Solution
| Project input | What we need from you | How we use it |
|---|---|---|
| Mill identification | Make, model, shell diameter and effective grinding length | Pattern matching, plate count, curvature |
| Operating data | Speed and percent critical, charge level, ball size and charge mass, motor power | Lifter profile, spacing, face angle |
| Ore and duty | Feed size, work index, abrasiveness, moisture | Alloy family and heat-treatment route |
| Existing hardware | Drawings, worn samples, 3D scan, bolt and hole details | Geometry confirmation before pattern work |
| Site constraints | Crane capacity, mill door size, change-out window | Piece weight split, delivery and packing scope |
| Wear history | Previous liner life, failure mode, thickness records | Grade and profile revision for the next campaign |
Packing is arranged by liner type with lifting points and edge protection, and delivery scope is confirmed as individual castings, a complete shell set or a full mill liner package including grate and pulp lifter castings. Drawings, test records and installation documentation are issued in the language agreed at order stage.
Frequently Asked Questions
Can you produce SAG mill liners from our existing drawings or worn components?
Yes. We work from mill drawings, OEM part numbers, worn liner samples or a laser scan of the shell and end walls. Geometry is confirmed with a layout drawing before pattern and mold preparation, and we flag any bolt-hole or chord-length deviation for sign-off.
How do you choose between high-chromium cast iron and manganese steel for a SAG liner?
It follows the duty of the position. Abrasion-dominated shell zones suit high-chromium grades; feed-end and other high-direct-impact positions generally favour work-hardening manganese steel or a composite arrangement that combines a hard wear face with a ductile backing.
What documents accompany a liner shipment?
Each order is supplied with a packing list, heat-number traceability, chemical composition and hardness records from our testing room, dimensional inspection results and a position-marked installation layout. Certification for ISO9001, ISO14001 and ISO45001 is maintained at company level.
What casting sizes and output can you support for a complete mill liner package?
Our heavy casting capability covers pieces up to 5000 × 5000 × 1000 mm within a 1500 kg single-piece limit, and thick compact castings to 1500 × 1500 × 1200 mm at up to 3000 kg. Annual output of cast balls and castings is 60,000 tons, which supports shell sets, head liners, grates and pulp lifters in one campaign.
Do you supply replacement liners to the same specification later in the mill's life?
Patterns and process records are retained, so replacement castings are produced on the same alloy and heat-treatment route as the original set. Where wear records show a change in the dominant failure mode, we revise the grade or profile at that point rather than repeating the previous design unchanged.
Can you supply grinding media for the same SAG and ball mill circuit?
Yes. We cast high-chromium, medium-chromium and low-chromium grinding balls from Ф8 mm through Ф150 mm alongside our liner range, so media and liner selection can be coordinated to the same ore, charge and throughput target.



