


 English
 русский
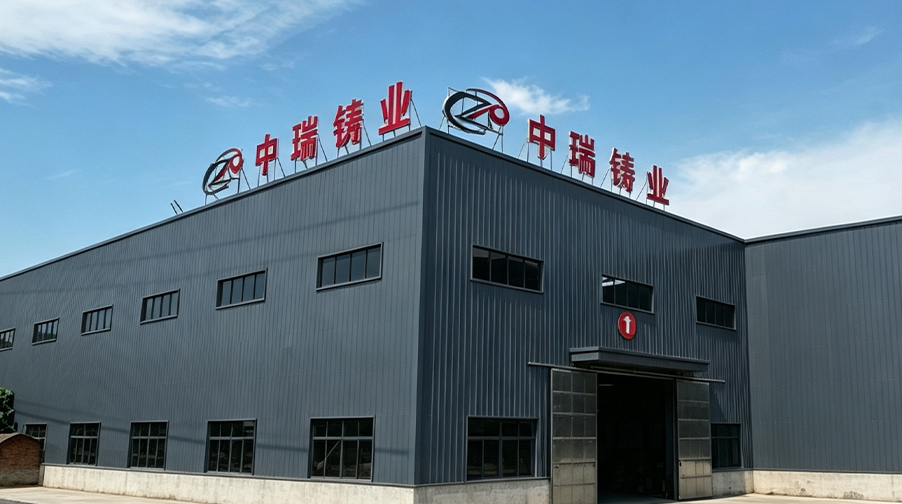
Anhui Ningguo Zhongrui Wear-Resistant Materials Co., Ltd. casts Casting Vertical Mill Liner manufacturer components for vertical roller mills in cement, slag, coal and mineral grinding circuits. Our work starts from the wear track: table liner segments, roller tires and sleeves, nozzle ring castings, dam ring and retainer plates, and the bolt-on liners that protect the mill body. Melting, moulding, heat treatment and inspection run inside our own workshops in Ningguo City, Anhui Province, so the alloy and the profile stay under one production team from pattern to packed set.
A vertical mill grinds by pressure and attrition rather than by a tumbling charge, so its liner set behaves as a matched system instead of a list of plates. We cast segments as a set to the attachment geometry the grinding table already has, which keeps the changeout on the mill's normal downtime window and avoids re-drilling on site.
What Our Vertical Mill Liner Range Covers
The material bed forms in the middle of the table, spreads outward across the grinding track and leaves through the nozzle ring. Each position therefore sees a different mix of pressure, abrasion and temperature, and we cast for those zones separately.
- Grinding table liner segments — the segmented ring bolted to the table, cast with flat, stepped, grooved or wave profile and with counterbored seats matched to the existing bolt circle.
- Grinding roller tires and roller sleeves — the rotating wear body pressed onto the bed; edge geometry and alloy are set by the impact the roller meets at the material inlet.
- Nozzle ring segments and air-guide castings — they govern the gas velocity that lifts ground material and wear quickly when recirculation or feed coarseness rises.
- Dam ring, retainer ring and table edge castings — they control bed depth and normally take a tougher grade than the grinding track because edge impact dominates.
- Classifier blades, separator liners and housing or door liners — bolt-on protection for the static parts of the mill.
- Castings to drawing — where an OEM part is no longer economic, we work from the customer's drawing or from a worn sample taken off the mill.
Materials and the Casting Route Behind Each Zone
Alloy selection follows the wear mechanism rather than one universal best grade. An abrasion-dominated table track behaves differently from a roller edge that takes repeated high-pressure impacts, and a coal mill with hot gas flow is not the same duty as a raw meal mill.
| Material direction | Typical position in the mill | Wear behaviour it is chosen for |
|---|---|---|
| High-chromium cast iron | Table liner segments, roller tires | Sliding abrasion on the grinding track, profile retention on fine grinding |
| Medium-chromium alloy steel | Large table segments, dam ring, structural liners | Balanced abrasion resistance and toughness under load peaks and thermal cycling |
| High-manganese steel | Roller edges, nozzle ring, impact-heavy zones | Surface work-hardening where grinding pressure and coarse feed create impact |
Profiled segments and roller tires with internal cavities are produced on our fully automatic lost foam vacuum precision casting line; heavier and simpler liner blocks run through resin-sand moulding or the automatic iron mould sand-coating lines. Heat treatment completes the material decision: the automatic quenching and reheat line and two automatic flipping annealing furnaces let us build an abrasion-resistant structure while keeping the toughness the mill needs at start-up and at load peaks.
Critical Specifications We Confirm Before Casting
Geometry, attachment and duty data are fixed before a pattern is made, because a vertical mill liner that fits but grinds badly costs more than a late delivery.
- Mill make and model, table diameter and roller diameter or width, taken from the general arrangement drawing or the OEM manual.
- Segment count, bolt circle, bolt size and counterbore depth — these must match the table without on-site re-drilling.
- Wear profile: replicate the profile currently in service, or deepen the track where the mill has grinding capacity to spare.
- Alloy and hardness target, plus any chemistry limits that apply to the customer's own specification.
- Single-piece weight against site crane capacity and the largest piece that will pass the mill door.
- Operating data: throughput, feed size, product fineness, grinding pressure, moisture and mill outlet temperature.
- Quantity and phasing: first fill, one spare set, or a rolling programme that supplies the highest-wear zone on its own cycle.
Melting, Heat Treatment and Inspection
Every heat is melted in our VIP-1800 series furnaces under temperature control and analysed before and after melting on a direct-reading spectrometer that checks more than a dozen elements. If a reading drifts from specification, the heat is corrected before pouring rather than after casting. A carbon-sulfur analyzer covers the carbon balance, and far-infrared measurement holds the pouring temperature as the mould fills.
After shakeout and cleaning, each casting passes a first visual inspection: a sound surface free of cracks, slag inclusions, pores, sand holes, shrinkage cavities and cold shuts. Approved pieces move on to grinding and finishing, then to hardness testing and dimensional check against the drawing.
- Chemical composition record for the heat
- Hardness results from the tested positions
- Dimensional record covering bolt pattern, thickness and profile
- Piece weight and identification marking
- Inspection sign-off before packing and dispatch
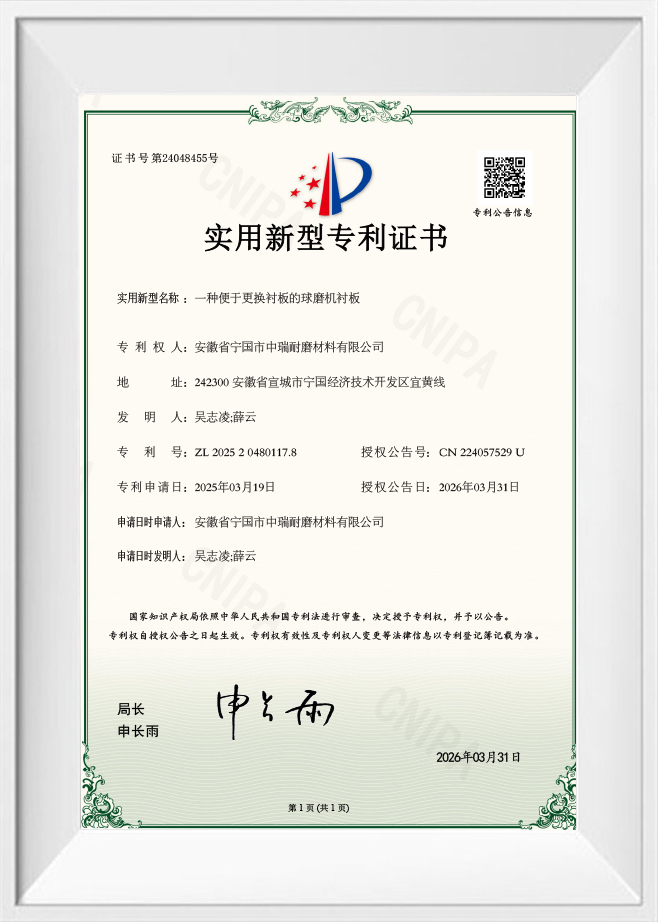
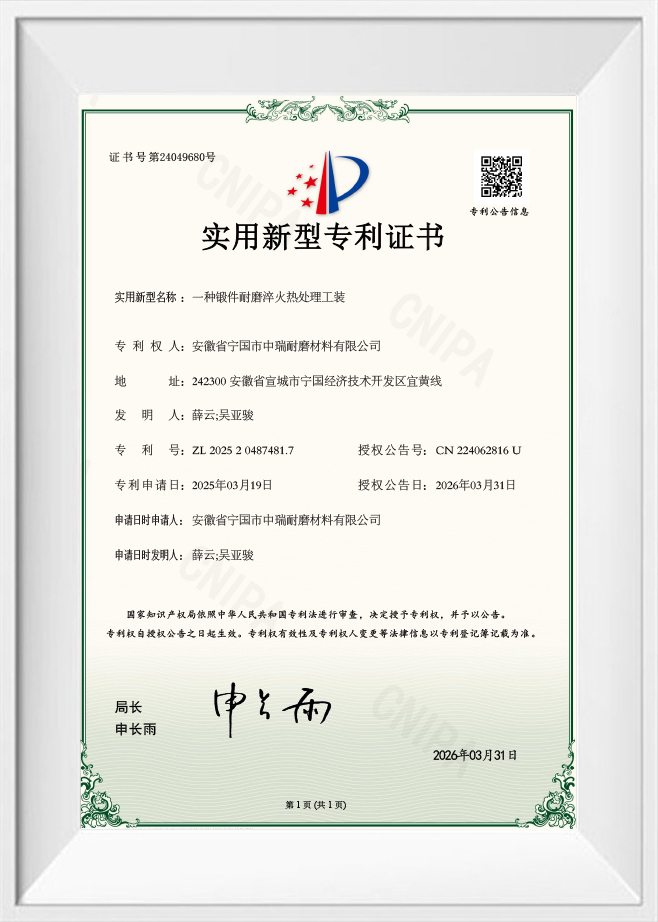
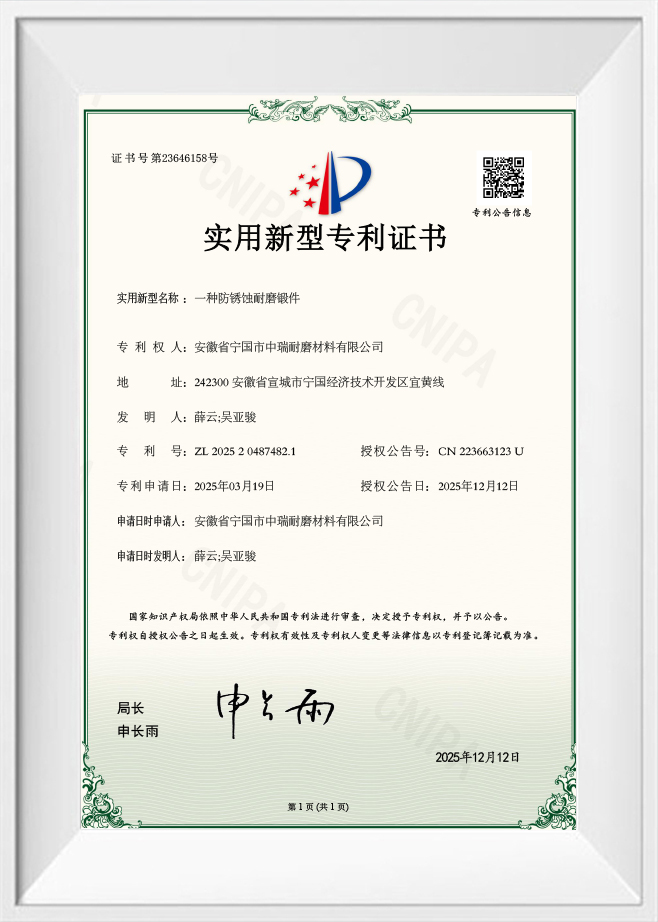
Our management system is certified to ISO9001, ISO14001 and ISO45001, and the plant holds Safety Production Standardization certification together with utility model patent certificates from development work on casting equipment.
Installation, Commissioning and Wear-Life Support
Liner life depends on installation as much as on the casting. Seating surfaces have to be clean and flat, bolts torqued in the sequence the mill manual gives, and the roller-to-table gap set to suit the bed depth that the grinding pressure requires.
- Fasteners quoted with the liner order where the customer's bill of materials calls for a complete set.
- Nozzle ring clearance and classifier settings checked before first feed, since both change recirculating load and outer-track wear.
- Segment rotation or reversal after a measured wear interval, to even the track and push back the changeout.
- Wear mapping at fixed measuring points, so the next set is ordered against real thickness data rather than a calendar.
- Lifting points cast or marked on heavy pieces, with packing arranged for the transport mode and the port of discharge.
Information We Use to Configure Your Solution
Our proposal is built on the working point of the mill and the attachment it already has. The table below shows the inputs that change the casting, the alloy or the price, and how each one is used.
| Input we need | What it decides |
|---|---|
| Mill model, table and roller dimensions | Segment count, arc length, profile radius and total set weight |
| Existing liner drawing or worn sample | Bolt circle, counterbore depth, thickness build-up and interchangeability |
| Feed material, throughput and product fineness | Alloy direction, hardness target and track profile |
| Grinding pressure and mill outlet temperature | Toughness requirement and heat treatment cycle |
| Quantity, spare policy and destination | Pattern planning, packing method, marking and delivery scope |
Where This Fits in Our Casting Range
Vertical mill liners sit alongside the rest of our Casting Mill Liner family, which covers grinding equipment across the comminution line.
Table segments, roller tires, nozzle ring, dam ring and static wear plates for cement, slag, coal and mineral VRMs.
Shell and end liner plates for horizontal ball mills, including Mn13Cr2 and Mn-Cr alloy steel and high manganese grades.
Heavy-section liners and composite arrangements for semi-autogenous mills where impact dominates.
Beyond the mill liner family we cast grinding media, crusher wear castings and general steel castings, which lets a grinding circuit be equipped from a single foundry with one set of composition and hardness records.
Frequently Asked Questions
Which vertical mill liner parts do you cast?
Table liner segments, grinding roller tires and sleeves, nozzle ring and air-guide castings, dam and retainer ring castings, classifier blades, separator and housing liners, plus special castings produced to a customer drawing or a worn sample.
How do you choose the alloy for a table liner or roller tire?
We read the wear mechanism first. Abrasion-dominated grinding tracks go to high-chromium cast iron; large segments and dam rings where load peaks and thermal cycling matter go to medium-chromium alloy steel; impact-heavy roller edges and nozzle rings go to high-manganese steel. The final grade is fixed together with the hardness target after we see the operating data and the failed part.
Can you match an existing profile, bolt pattern and counterbore?
Yes. Working from a drawing or a sample, we reproduce the bolt circle, counterbore depth, thickness and track profile so the set drops onto the existing table. Where a mill has spare grinding capacity, we can also quote a deeper or differently stepped profile to extend the wear interval.
What do you need to quote a vertical mill liner set?
Mill model and dimensions, the existing liner drawing or sample, required alloy or hardness, feed material and product fineness, grinding pressure and mill temperature, quantity and spare policy, and the delivery destination. With those inputs we return a set list, piece weights and a casting programme.
How is quality verified before shipment?
Pre-melt and post-melt spectrometer analysis, carbon-sulfur determination, far-infrared pouring temperature control, controlled quenching and annealing, visual rejection of cracks, pores, sand holes, shrinkage and cold shuts, then hardness testing and dimensional check against the drawing.
What casting capacity and delivery scope do you offer?
Our foundry runs an annual capacity of 60,000 tons of cast balls and castings across casting, mould cutting, heat treatment, raw material, finishing and physical testing workshops. Large liners can be cast in heavy single pieces, and heavy machined castings are produced in our dedicated casting bay, with packing arranged around the transport mode and unloading equipment at site.



