


 English
 русский
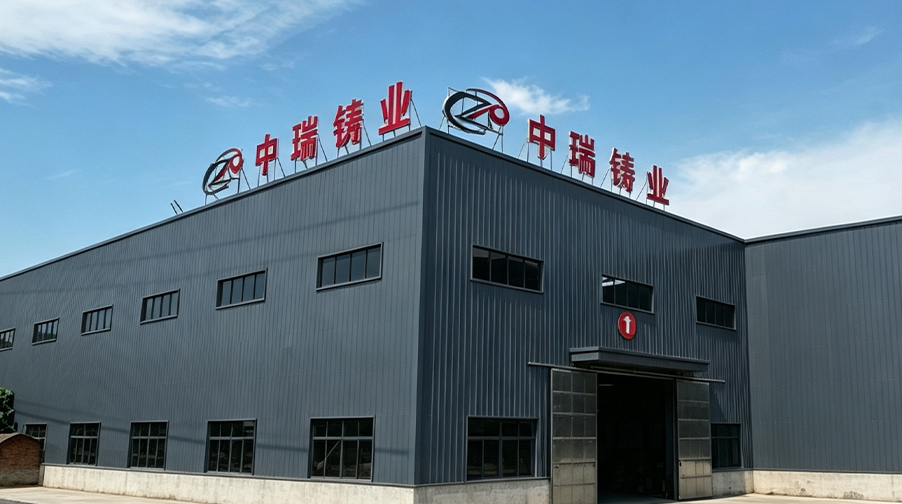
Anhui Ningguo Zhongrui Wear-Resistant Materials Co., Ltd. is a Casting Bucket Tooth manufacturer working from Ningguo City, Anhui Province, China, where we cast alloy steel bucket teeth and matching adapters for excavators, wheel loaders and mining shovels. Melting, moulding, heat treatment and inspection sit inside our own plant, so alloy grade, nose geometry and hardness are controlled as one production sequence instead of being stitched together across subcontractors.
Bucket teeth belong to our Casting Wear Parts for Mining Equipment family, which also covers classifier blades, crusher wear castings and grinding media for the same mining, quarry, coal and cement flows. A digging assembly is treated as a set: tip, nose, pin and retainer pocket are measured together against the machine the bucket is fitted to.
Casting Bucket Tooth and Adapter Range
Two parts of a bucket assembly wear on different schedules. The tip does the cutting and takes the sharpest abrasion; the adapter transfers digging force into the bucket lip and stays on the machine through several tip changes. We cast both, which keeps nose fit, pin bore and tip seat contact inside one set of tolerances.
- Cast bucket tips in standard digging, heavy-duty and narrow rock or chisel profiles.
- Casting Bucket Adapter bodies for weld-on and bolt-on bucket lips, cast to suit the lip thickness on the machine.
- Pin and retainer pocket geometry defined together with the nose, so the tip locks without shimming on site.
- Custom tooth forms cast from customer drawings, worn samples or field measurements.
| Product | Form | Typical fit | Wear duty | Material direction |
|---|---|---|---|---|
| Standard digging tooth | Pin-on tip, straight or tapered nose | Excavators and loaders in soil, gravel, sand, coal | Even abrasion, moderate impact | Medium-chromium alloy cast iron, alloy steel |
| Rock / chisel tooth | Pin-on tip, narrow penetrating profile | Hard rock, overburden, quarry shot rock | High impact combined with abrasion | High manganese steel, bimetallic composite casting |
| Heavy-duty wide tooth | Pin-on tip, wide blunt profile | Bulk handling, coal, slag, stockpile reclaim | Sliding abrasion, lower impact | High-chromium cast iron |
| Bucket adapter | Weld-on or bolt-on nose | Excavator and loader bucket lips carrying the tip | Lip abrasion, repeated load transfer | High-strength alloy steel |
| Custom tooth and adapter set | To drawing, sample or template | Non-standard buckets, grabs, dredging and special lips | Defined by the working point | Selected after reviewing the wear mechanism |
Application Fit Across Mining and Bulk Handling
Bucket tooth life is decided by the digging environment more than by the machine class. The same excavator loading blasted granite, river gravel or coal fines will consume a tip set at completely different rates, so the proposal starts from the working point rather than from a catalogue number alone.
- Open-pit and quarry loading: coarse, sharp, high-silica rock that drives abrasion and point loading on the tip nose.
- Underground and tunnelling loaders: confined faces, mixed ground and repeated scraping against the muck pile.
- Coal, lignite and stockyard duty: lower impact, longer sliding distances, wider teeth that clear sticky material.
- Cement, slag and clinker handling: hot, angular material that punishes both tip face and adapter shoulder.
- Cold-climate operations: impact behaviour of the alloy and retainer condition become the deciding factors.
For each enquiry we map machine size, bucket capacity, material type and target replacement interval before recommending a tip profile and an alloy grade. That mapping is what keeps a fleet from running an over-hardened tooth in high-impact ground or an over-tough tooth in fine abrasive sand.
Alloy direction follows the wear mechanism
- Abrasion-dominant ground: high-chromium cast iron gives the best resistance to scratching and metal loss on the tip face.
- Impact-dominant ground: high manganese steel work-hardens under repeated blows and resists cracking and chipping better than a very hard, brittle grade.
- Mixed duty: bimetallic composite castings position a hard wear zone where cutting happens while the body retains toughness at the pin and nose.
- Adapter bodies: high-strength alloy steel, because the adapter must survive the full life of several tips without deformation at the nose.
Casting Process and Dimensional Control
We operate three melting furnaces from the VIP-1800 series and cast through lost foam, iron mould sand coating and resin-sand shell moulding lines. Patterns and white moulds are cut in our own white mould cutting workshop, which shortens the loop between a new tooth drawing and the first cast sample. Heat treatment runs on automatic quenching and reheat lines with annealing furnaces, so hardness and internal structure are set by controlled cycles rather than by operator judgement.
- Temperature-controlled melting with spectrometer analysis before pouring.
- Constant-temperature pouring monitored by far-infrared temperature measurement.
- Automatic temperature-controlled quenching and annealing after casting.
- Cast envelope for larger adapter and lip components: individual castings up to roughly 5000 × 5000 × 1000 mm within a 1500 kg piece weight, and up to 1500 × 1500 × 1200 mm within 3000 kg, depending on the line used.
Dimensional work on teeth and adapters concentrates on the nose taper, pin bore, retainer pocket and tip seat. These are the features that decide whether a tip fits tightly on a customer's existing adapter, whether it rocks under load, and how quickly the assembly loosens in service.
Quality Control and Acceptance
Inspection runs alongside production rather than after it. Chemical composition is checked before and after each melt on a cabinet-type PRO spectrometer, with carbon-sulphur analysis and hardness testing supporting the release of finished castings from our physical property testing room.
- Pre-melt and post-melt chemical analysis, with composition corrected before pouring if it drifts from the agreed grade.
- Pouring temperature verified by far-infrared measurement.
- First visual inspection of each casting for cracks, slag inclusions, pores, sand holes, shrinkage cavities and cold shuts.
- Hardness testing on finished parts, with results recorded against the batch.
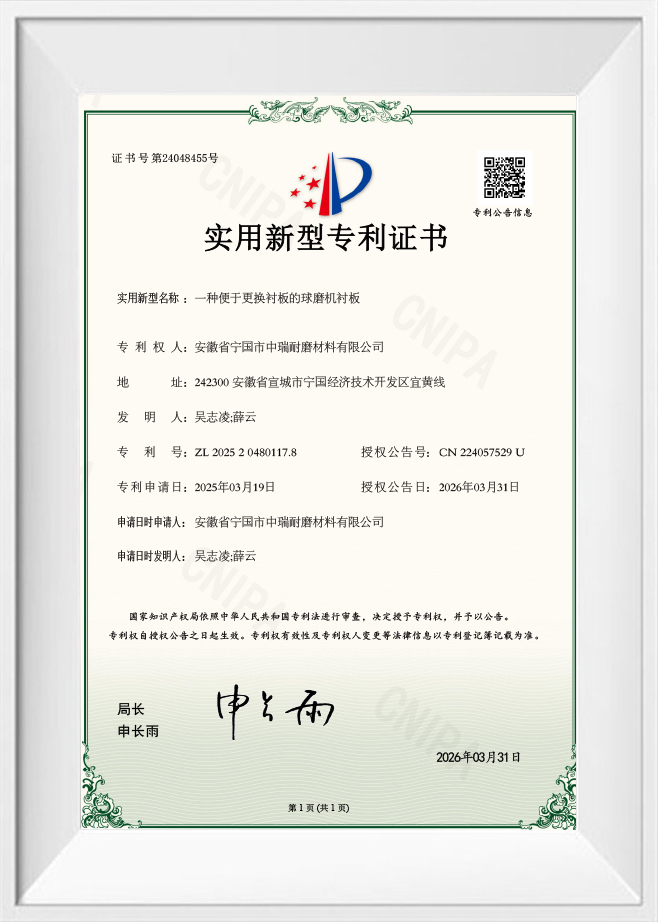
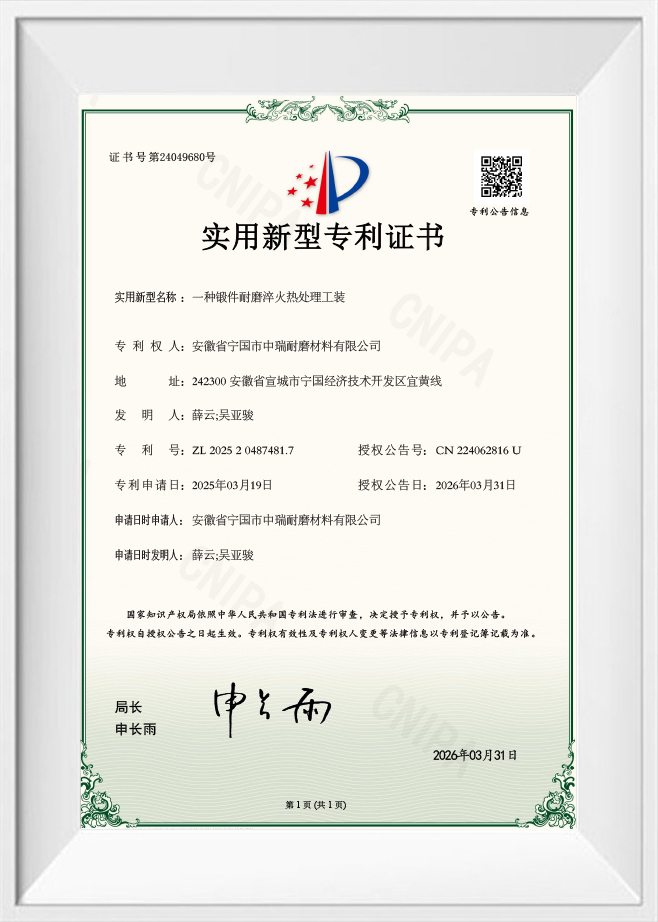
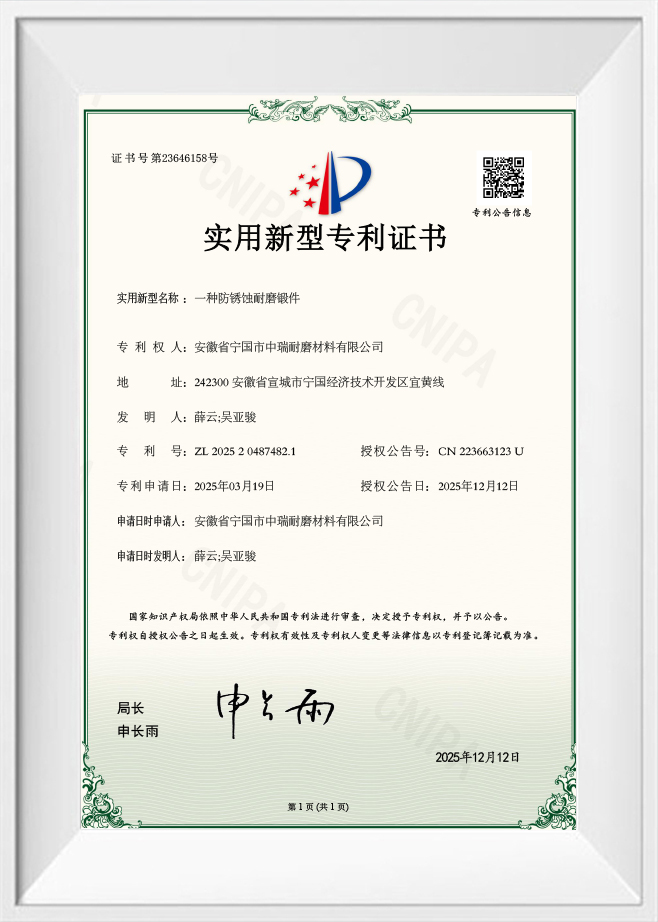
- Management systems certified to ISO9001, ISO14001 and ISO45001, plus Safety Production Standardization certification and utility model patent certificates held by the company.
Fitment, Installation and Fleet Wear Management
Bucket teeth are a consumable that has to fit hardware already in the pit, so fitment support is part of the supply. Where a customer runs mixed brands of buckets and adapters, we work from part numbers, drawings and measured dimensions so that one tooth number can serve several machines without site grinding.
- Fit check on nose taper, pin bore, retainer pocket and seat contact before shipment approval.
- Weld-on adapters supplied with the lip preparation and weld sequence agreed for the bucket material and plate thickness.
- Bolt-on adapters specified with fastener grade and tightening values for the installation crew.
- Wear limits expressed as a usable tip length, so maintenance crews know when to rotate or replace rather than run to failure.
- Spare-ratio planning for fleets that mix high-impact and high-abrasion faces in one pit.
Information We Use to Configure Your Solution
A workable tip-and-adapter proposal needs a defined working point. The more of the following we receive with an enquiry, the more precisely we can select the profile, alloy and heat treatment before a pattern is cut.
| Input | Why we need it | What it determines |
|---|---|---|
| Machine make, model and bucket type | Establishes digging force and bucket geometry | Tooth size class and tip mass |
| Existing part number, drawing, sample or measured dimensions | Confirms the interface that must be matched | Nose taper, pin bore, retainer pocket, tip length |
| Material being dug or loaded | Identifies abrasion versus impact balance | Alloy grade and profile selection |
| Fragment size, moisture and temperature | Shows whether the ground is coarse, sticky or hot | Profile width and material ductility requirement |
| Bucket lip thickness and weld access | Adapter attachment is fixed by the lip | Weld-on or bolt-on adapter design |
| Target service life and replacement interval | Sets the wear allowance to design for | Section thickness and usable tip length |
| Quantity, spare ratio and delivery destination | Drives scheduling, packing and shipping scope | Batch planning, packaging format and documentation |
Customization, Documentation and Delivery Scope
We are primarily a custom-focused foundry, and bucket teeth are a good example of why that matters: neighbouring pits with identical excavators often need different profiles and alloys. Customer drawings, worn samples and field measurements all feed the pattern shop, and the same melting and heat treatment disciplines apply to custom tips as to standard ones.
- New patterns and white moulds cut in-house for non-standard tooth and adapter forms.
- Gradual replacement planning for fleets that change a bucket line without stopping production.
- Inspection records drawn from spectrometer analysis and hardness testing, prepared with the shipment when requested.
- Packing arranged for the order size and route, including mixed consignments of tips, adapters and related wear castings.
- The same production base supplies crusher wear castings such as Casting Chromium Hammer parts and grinding media, so a mining site can consolidate wear-part supply across its crushing and loading circuits.
Frequently Asked Questions
Which excavators and loaders do your casting bucket teeth fit?
We match teeth and adapters to the machine model, the existing adapter part number and measured dimensions rather than to a single brand list. Send a drawing, a worn sample or the key measurements — nose width, pin bore, tip length and seat contact — and we confirm which of our castings will fit the bucket.
Which material should be used for hard rock digging?
Hard rock favours toughness over maximum hardness, so high manganese steel or a bimetallic composite casting is usually the better direction. Fine, sharp, highly abrasive material without heavy point impact suits high-chromium cast iron. We review the digging face, fragment size and cycle pattern before confirming a grade.
Can bucket teeth and adapters be cast to our own drawing?
Yes. Custom casting is our main mode of working. Drawings, samples, templates and site measurements go through our white mould cutting and casting workshops, and we return a dimensional check against the drawing before the batch is released.
How is quality controlled on a bucket tooth batch?
Each melt is analysed before pouring on a cabinet-type PRO spectrometer and corrected if the composition drifts. Pouring temperature is verified with far-infrared measurement, heat treatment follows a controlled quench and reheat cycle, and finished parts receive visual inspection for cracks, slag, porosity, sand holes, shrinkage and cold shuts plus hardness testing.
What information do you need for a quotation?
Machine model, bucket type, the interface dimensions or existing part number, the material being handled, the target replacement interval, order quantity and delivery destination. With those, we can propose a tip profile, an adapter design and an alloy grade, and quote the batch and packing scope together.
Do you supply adapters together with the teeth?
Yes. Tips and adapters are cast as a matched set so nose fit and pin bore relationships are controlled together. Where a customer already has adapters in service, we produce replacement tips to the existing interface and can verify fit before shipment.



