


 English
 русский
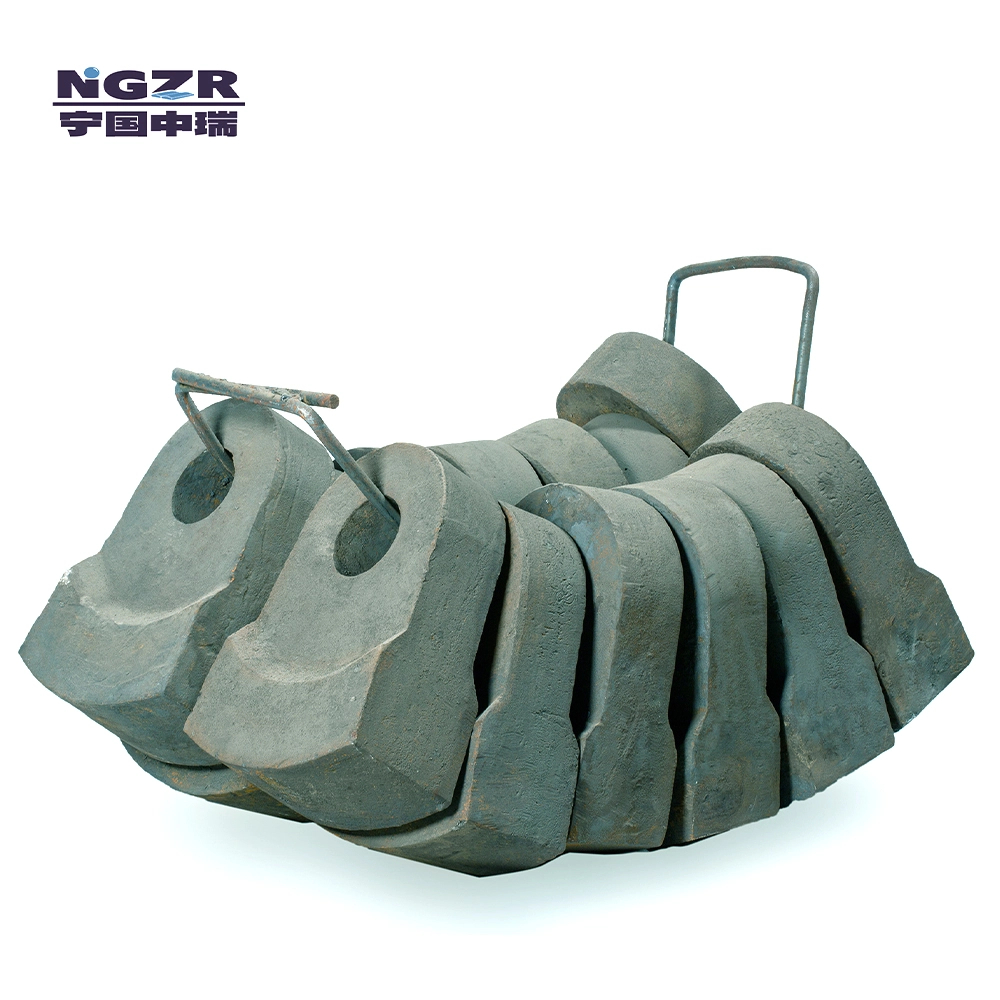
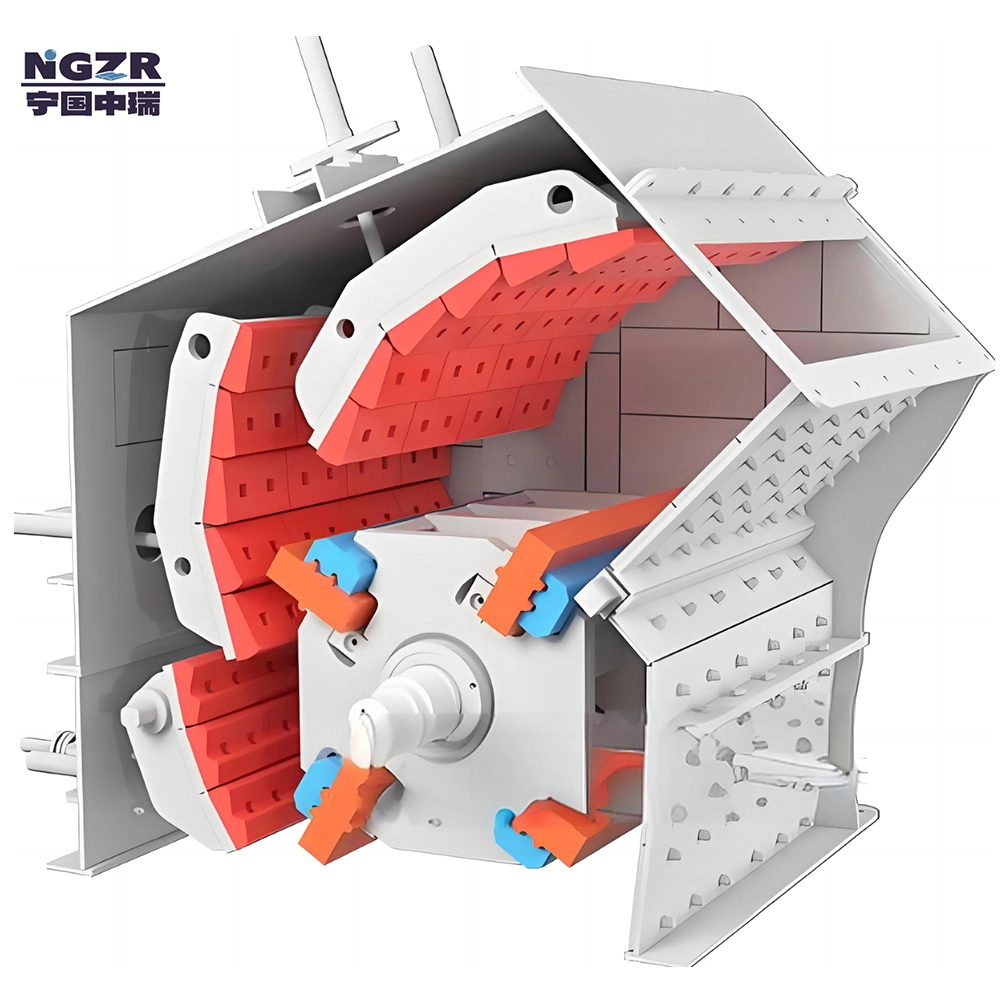
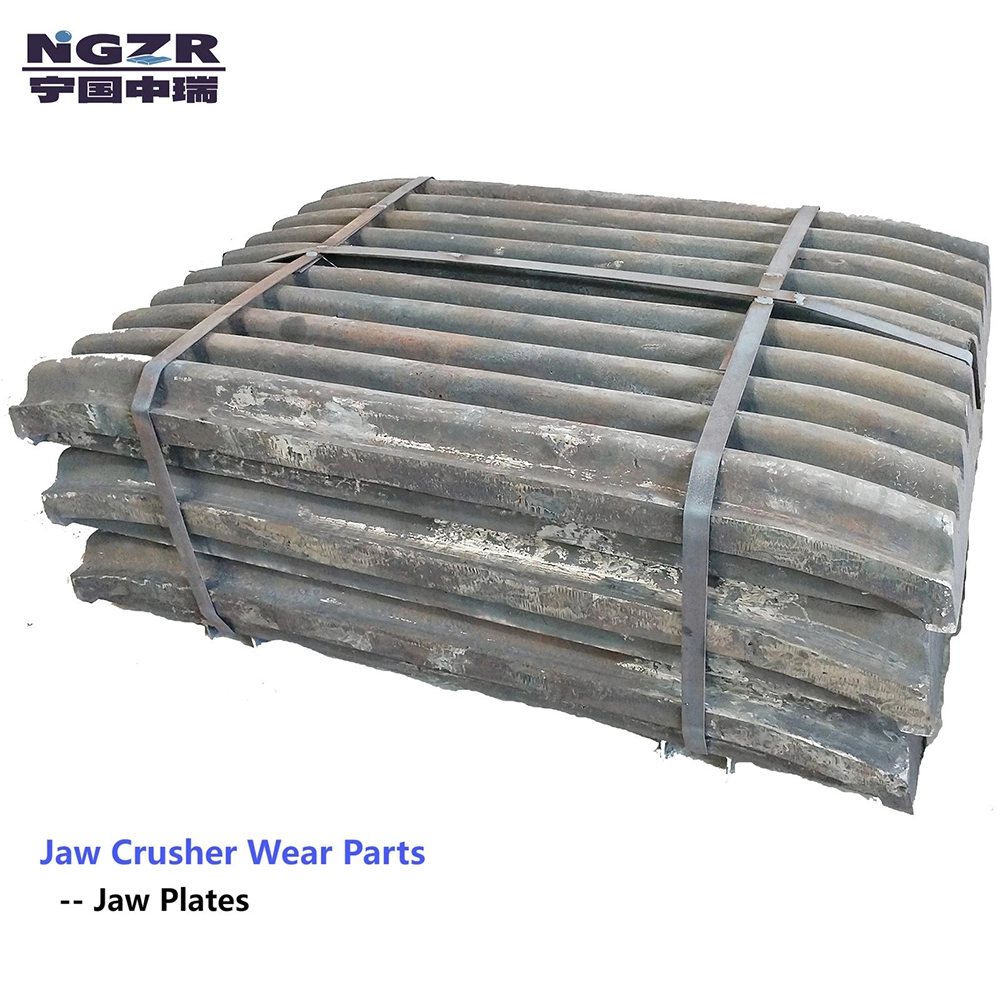
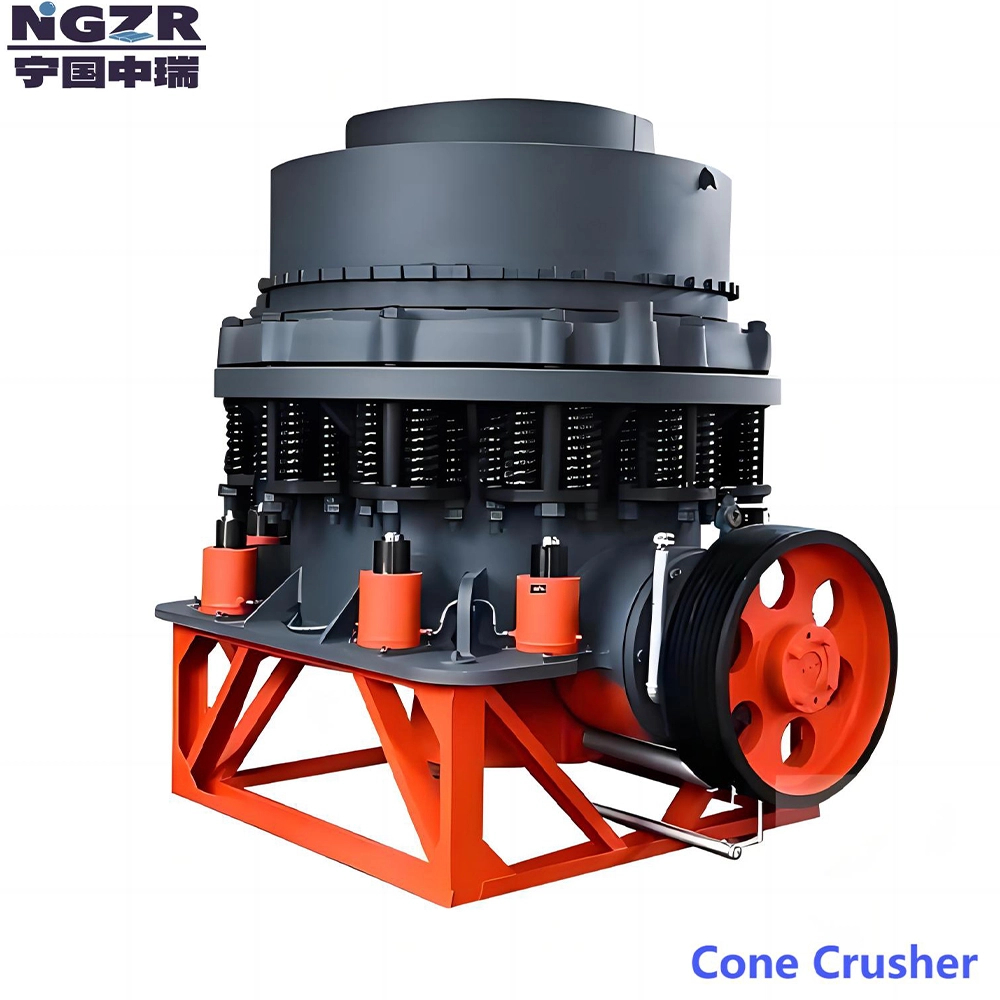
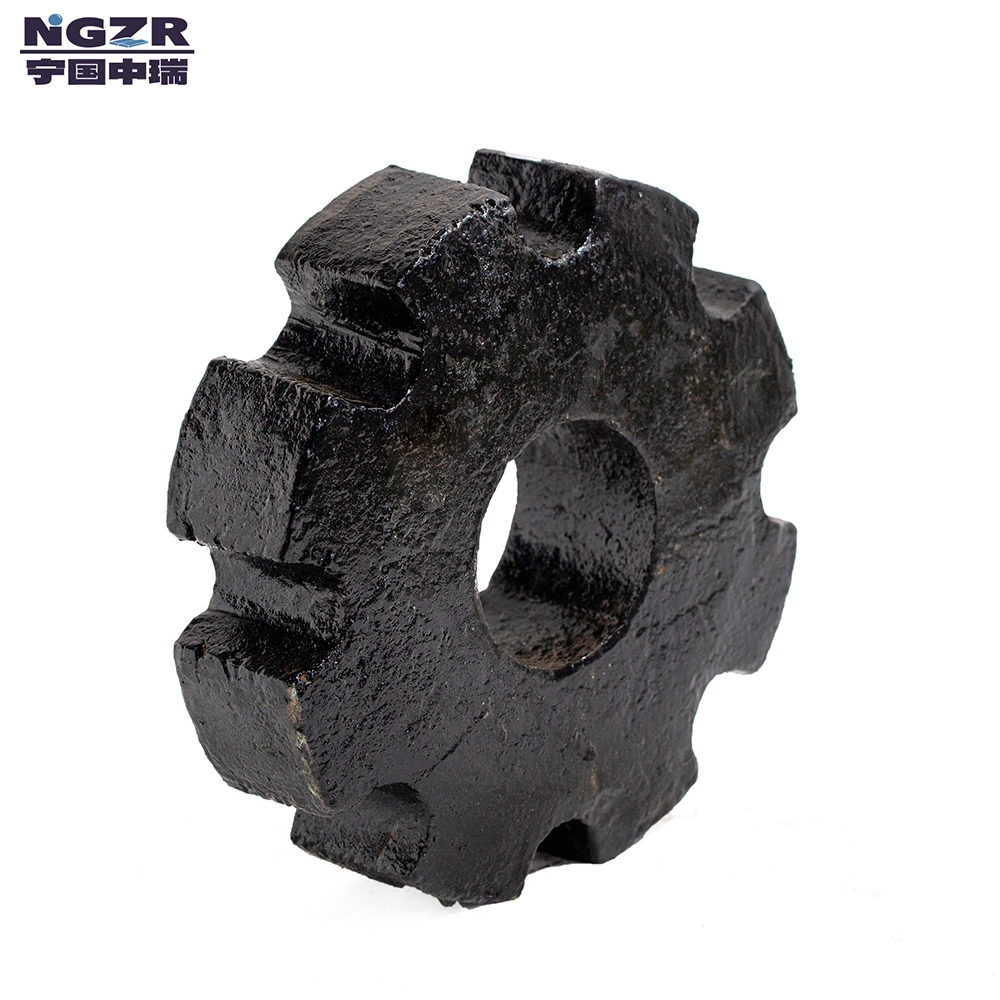
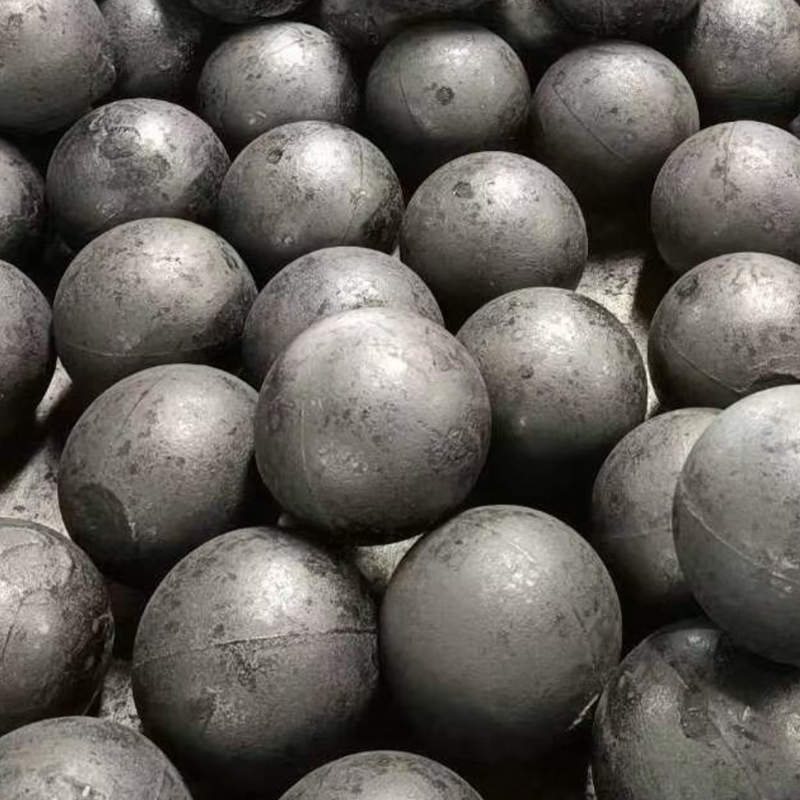
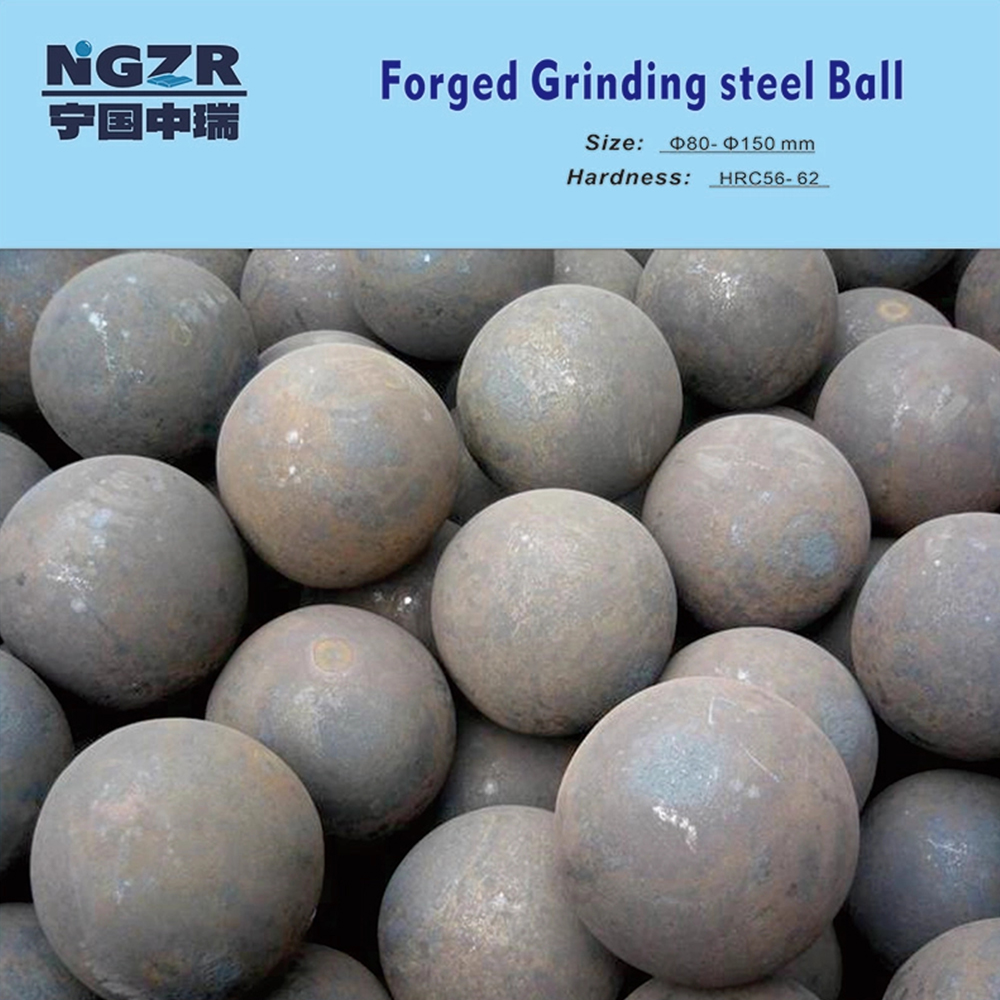
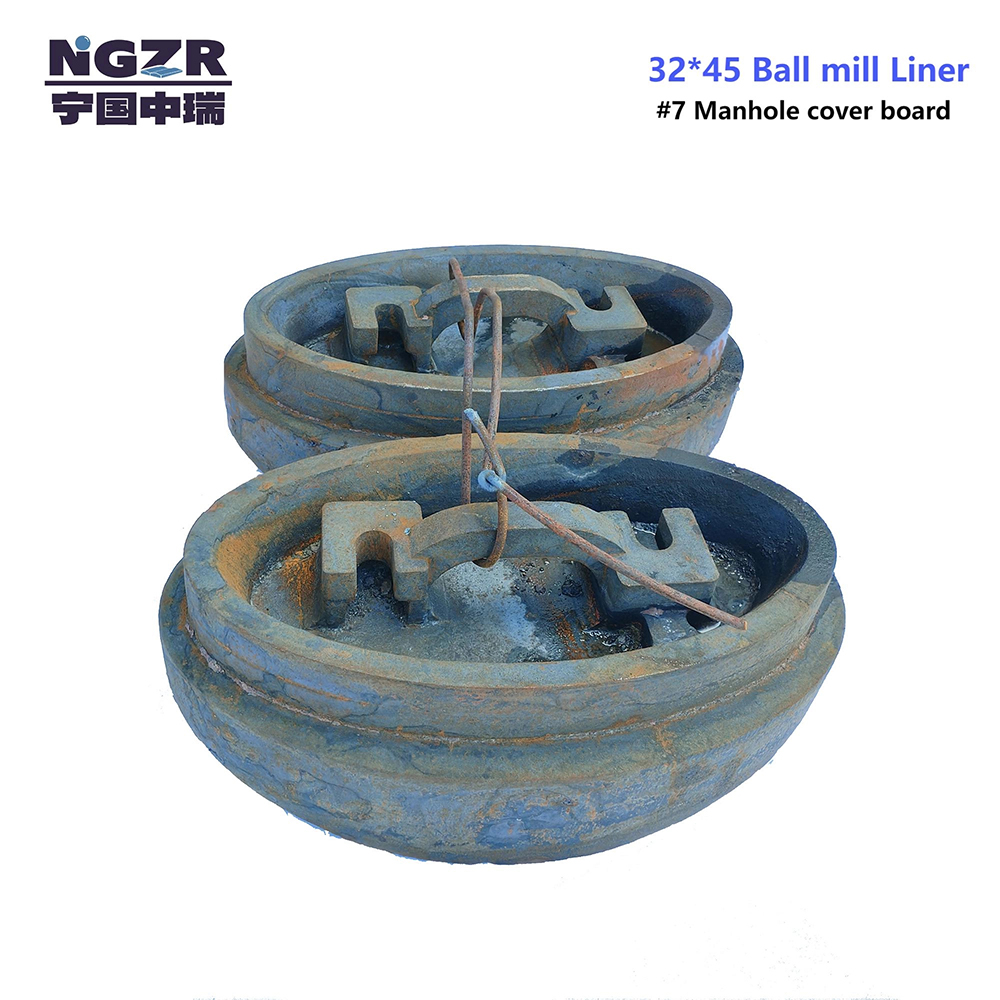
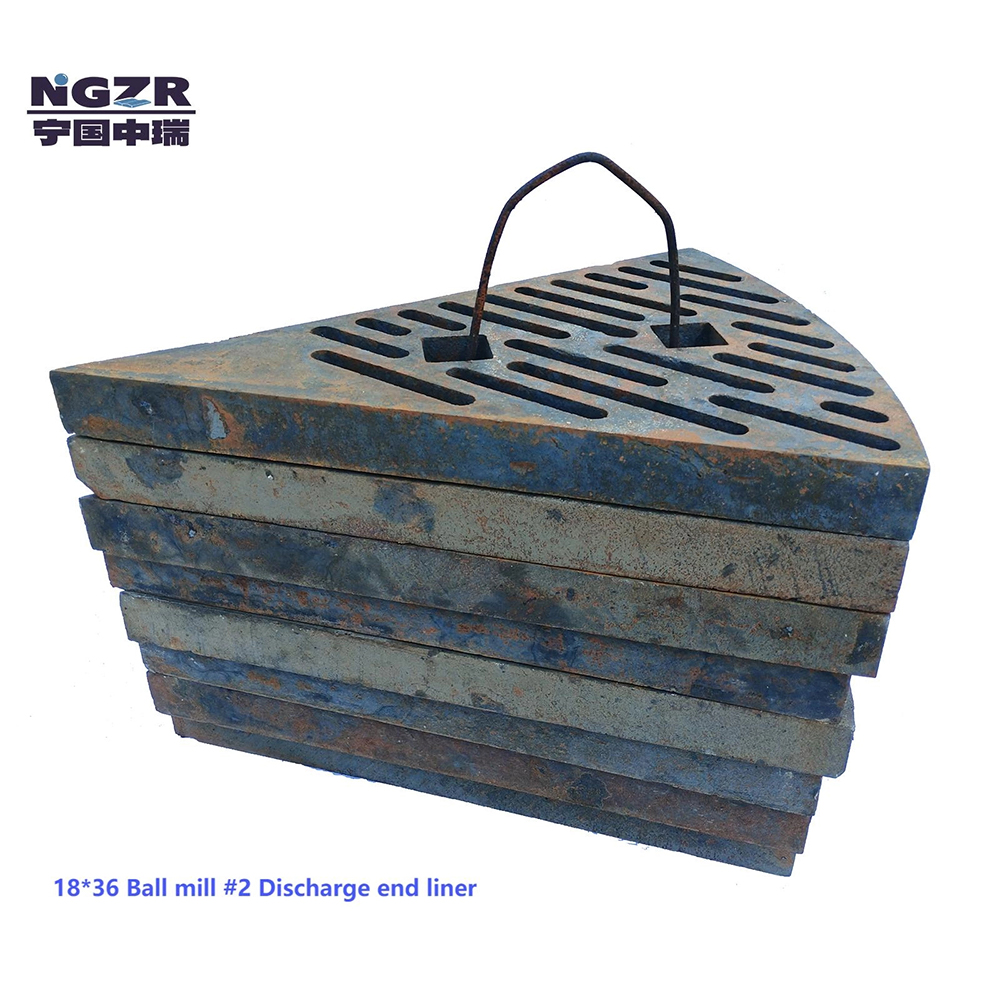
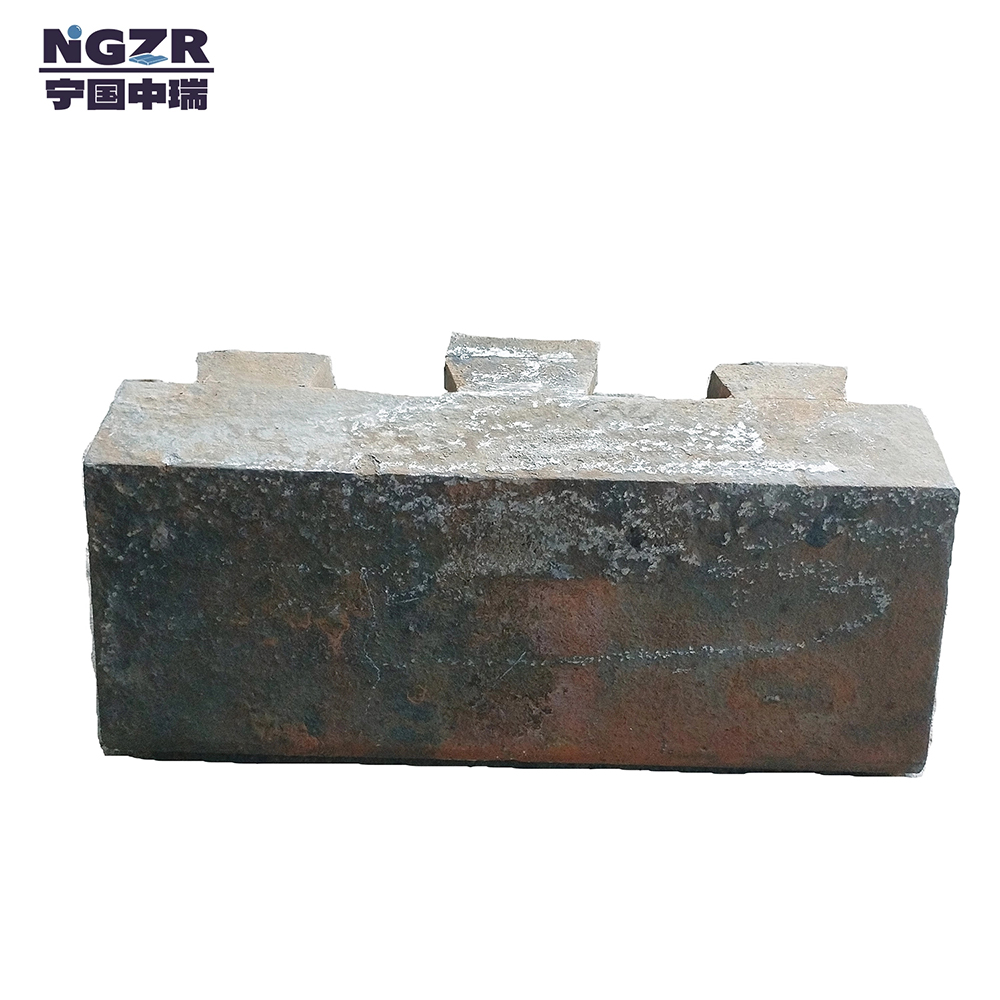
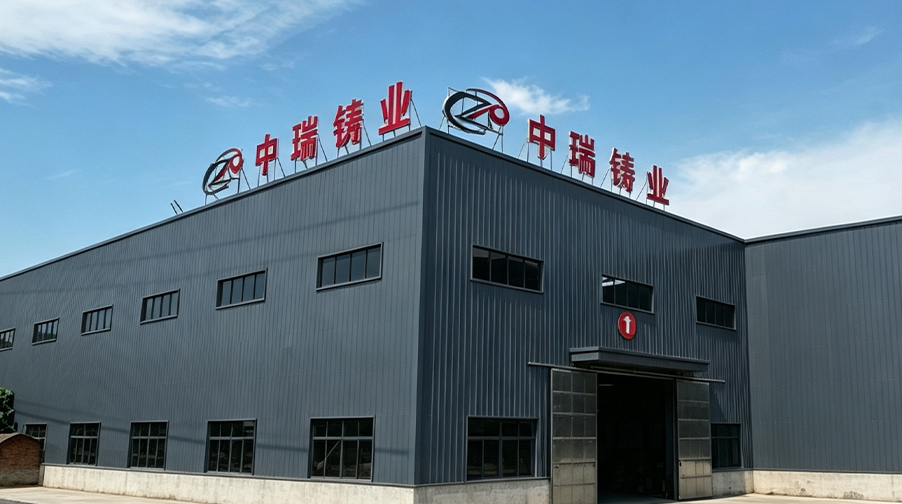
Anhui Ningguo Zhongrui Wear-Resistant Materials Co., Ltd. casts wear parts for crushing, grinding and mineral processing equipment at our foundry in Ningguo City, Anhui Province, China. Our Product range is organised into five casting families: crusher wear casting parts, casting grinding media, casting mill liners, casting wear parts for mining equipment and steel casting parts. High-chromium, medium-chromium and low-chromium alloy cast balls and cast sections, ball mill liners, crusher guards and hammers run through the same melting, pouring and heat treatment discipline.
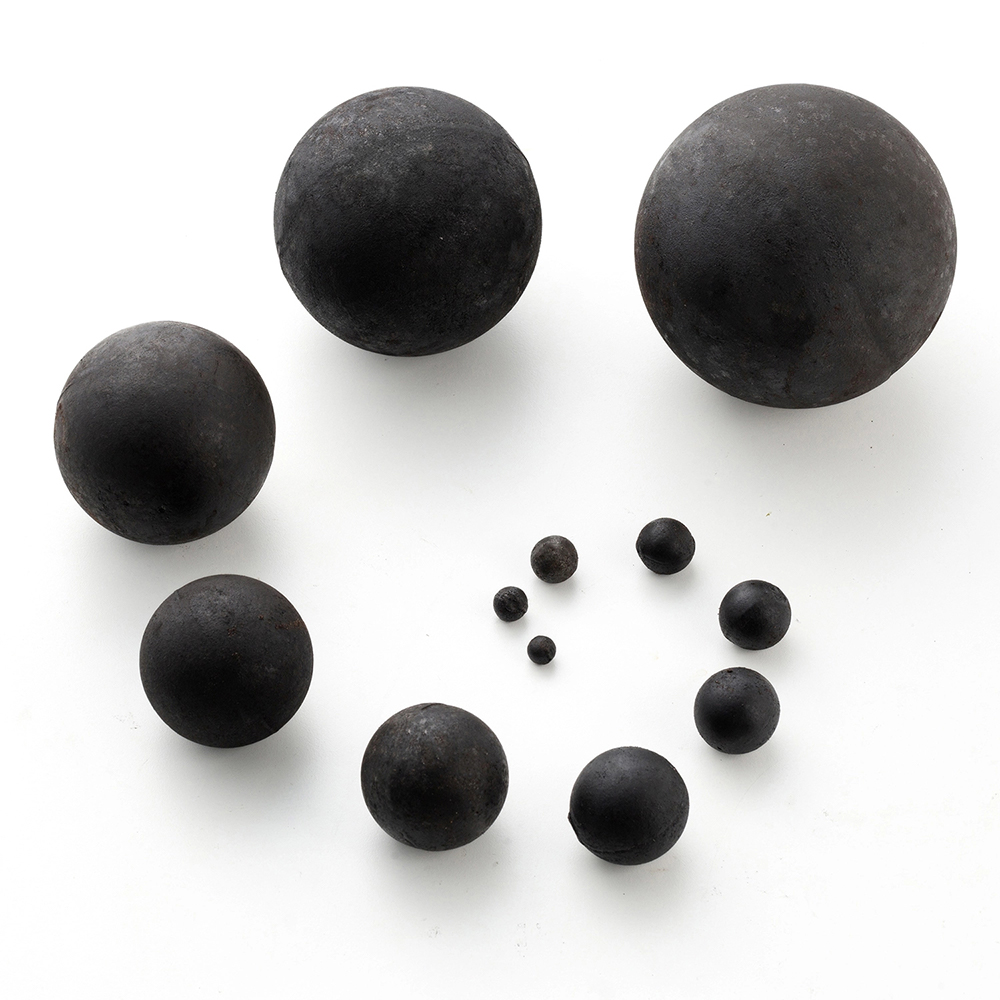
Annual output reaches 60,000 tons of cast balls and castings. Grinding media is produced from Ф8 mm to Ф150 mm; individual castings are made up to 5000 × 5000 × 1000 mm at up to 1,500 kg, or up to 1500 × 1500 × 1200 mm at up to 3,000 kg, depending on the moulding route. Cement, mining, thermal power, chemical and construction circuits are the application base for the whole range.
The Foundry Behind the Castings
Work is split across dedicated workshops — cast ball, casting, white-mould cutting, heat treatment, raw material, finished product and a physical property testing room. Temperature-controlled melting, constant-temperature pouring and automatic temperature-controlled quenching and annealing keep metallurgical results repeatable across a production campaign.
- 2 fully automatic iron mould sand coating production lines
- 4 robotic-arm shell moulding machines
- 1 fully automatic lost foam mould production line
- 1 fully automatic heat treatment quenching + re-tempering line
- 2 automatic flipping annealing furnaces
- 3 sets of VIP-1800 series melting furnaces
- Cabinet-type PRO spectrometer, carbon-sulfur analyzer, hardness tester and far-infrared temperature measuring instrument
Three casting routes are installed: resin-sand wooden mould manual casting, a fully automatic metal mould resin-sand shell mould vertical line, and a fully automatic lost foam precision casting line. Process selection follows part envelope, section thickness and order quantity, so large mill liners and heavy crusher guards can be scheduled alongside high-volume grinding media.
Our Casting Range and Where Each Product Fits
Crusher Wear Casting Parts
Crusher Wear Casting Parts cover the crushing and screening front end: chromium hammers and blow bars for impact crushers, jaw plates and cheek plates, cone mantle and bowl liner, shredder knife hammers and liners for scrap recycling, plus square steel flange bases, lock nuts and wear-resistant bolt assemblies. High-chromium cast iron, bimetallic composite casting and high manganese steel are used according to whether the duty is abrasion-dominated or impact-dominated.
Casting Grinding Media
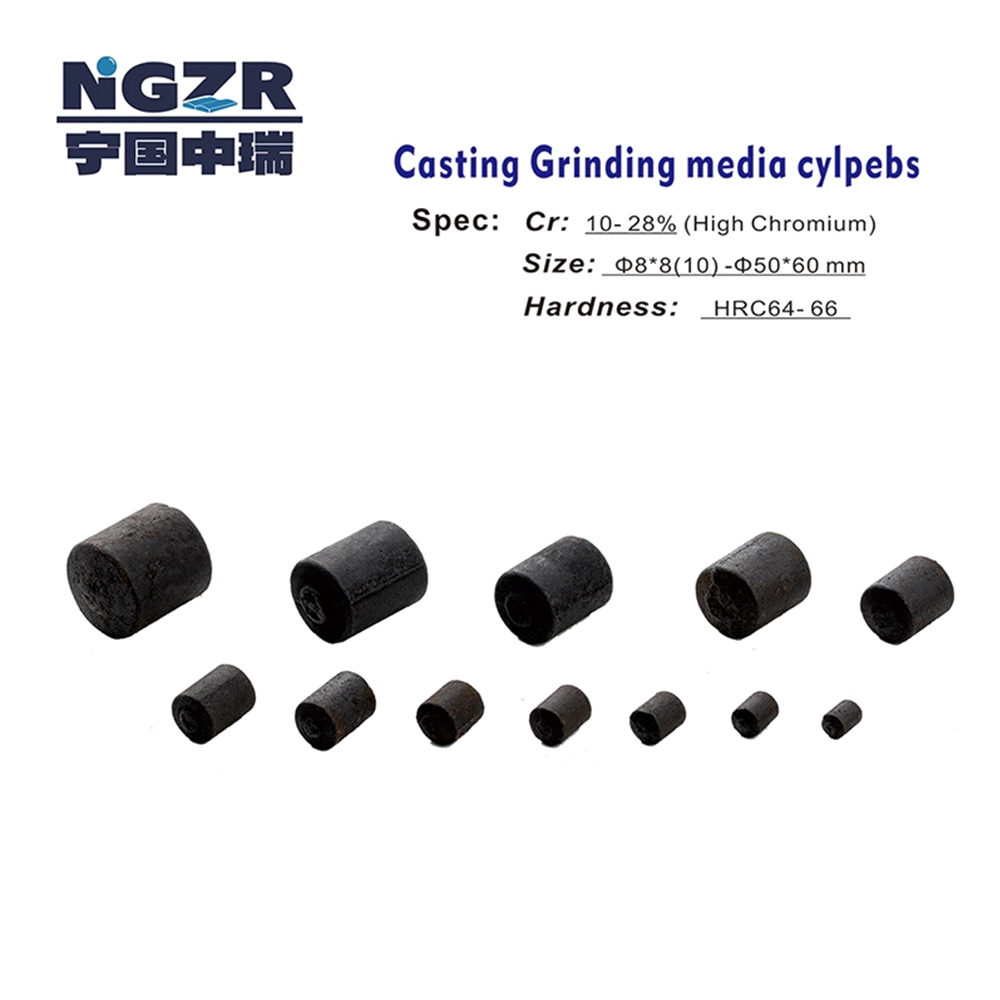
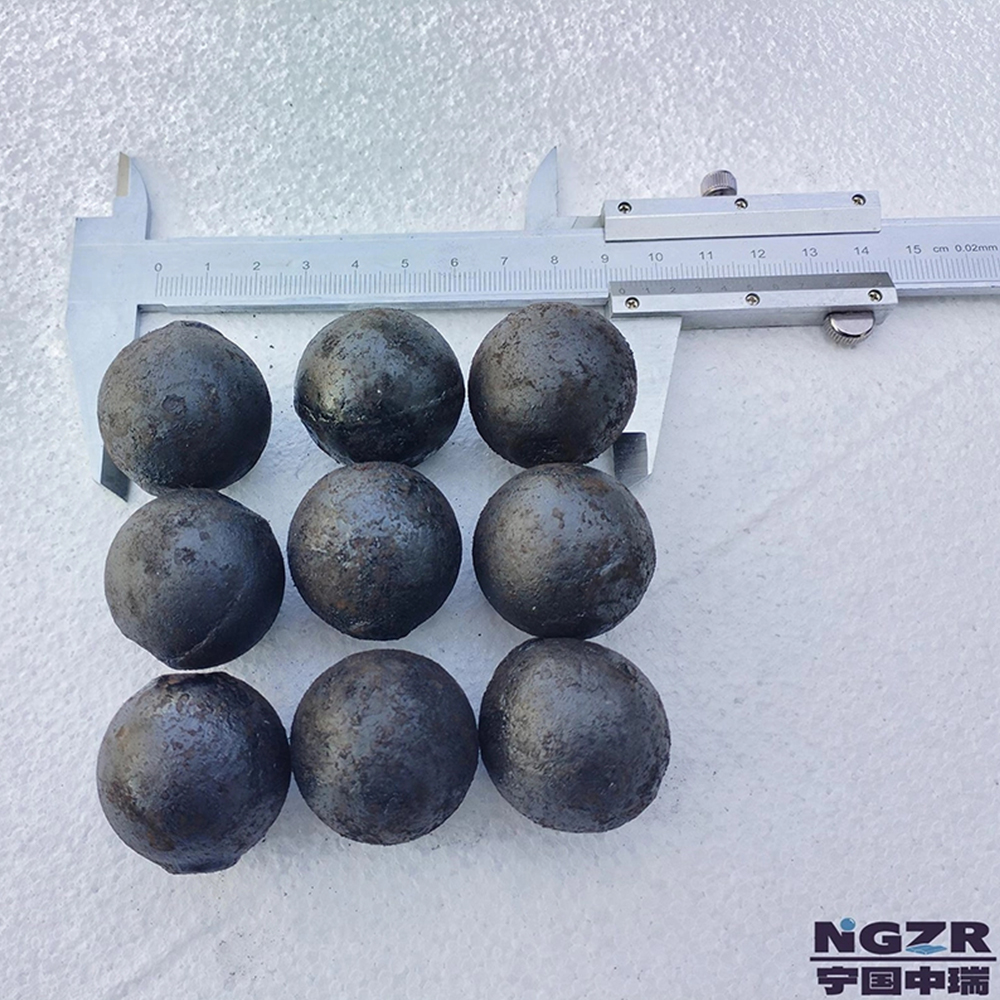
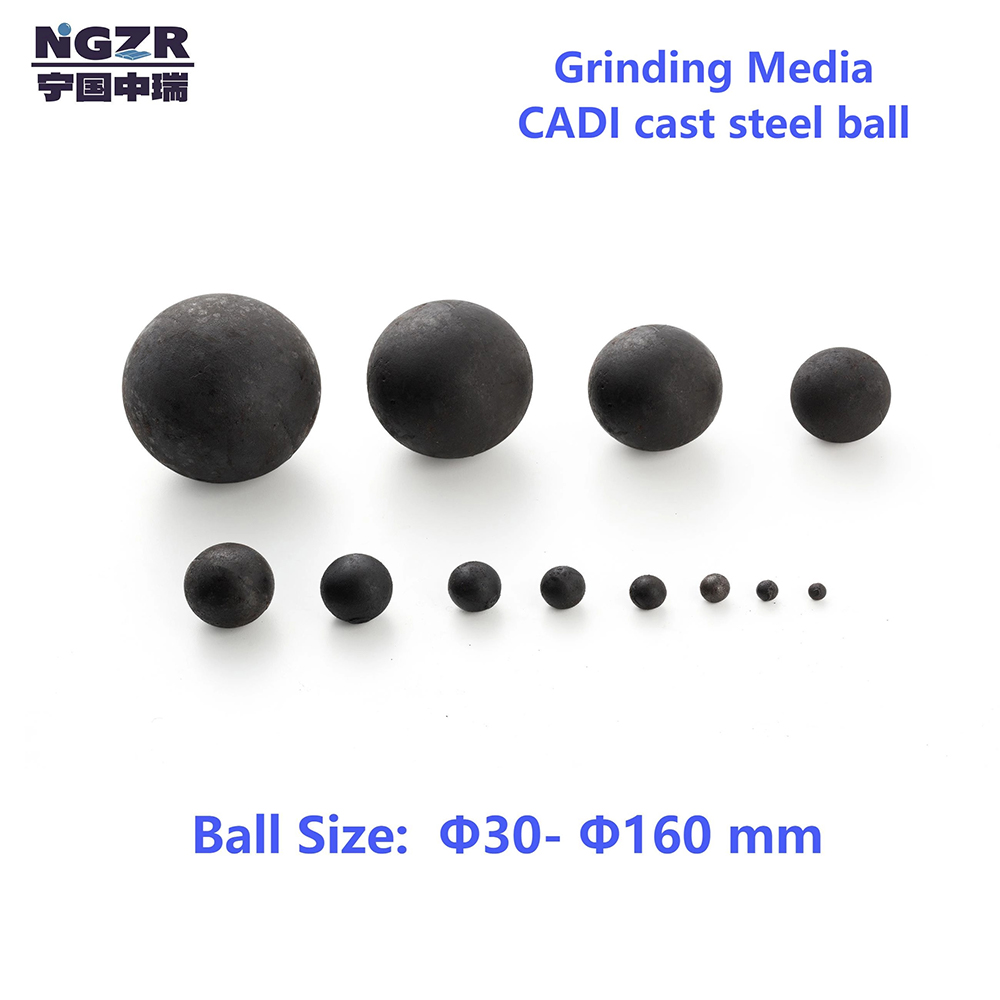
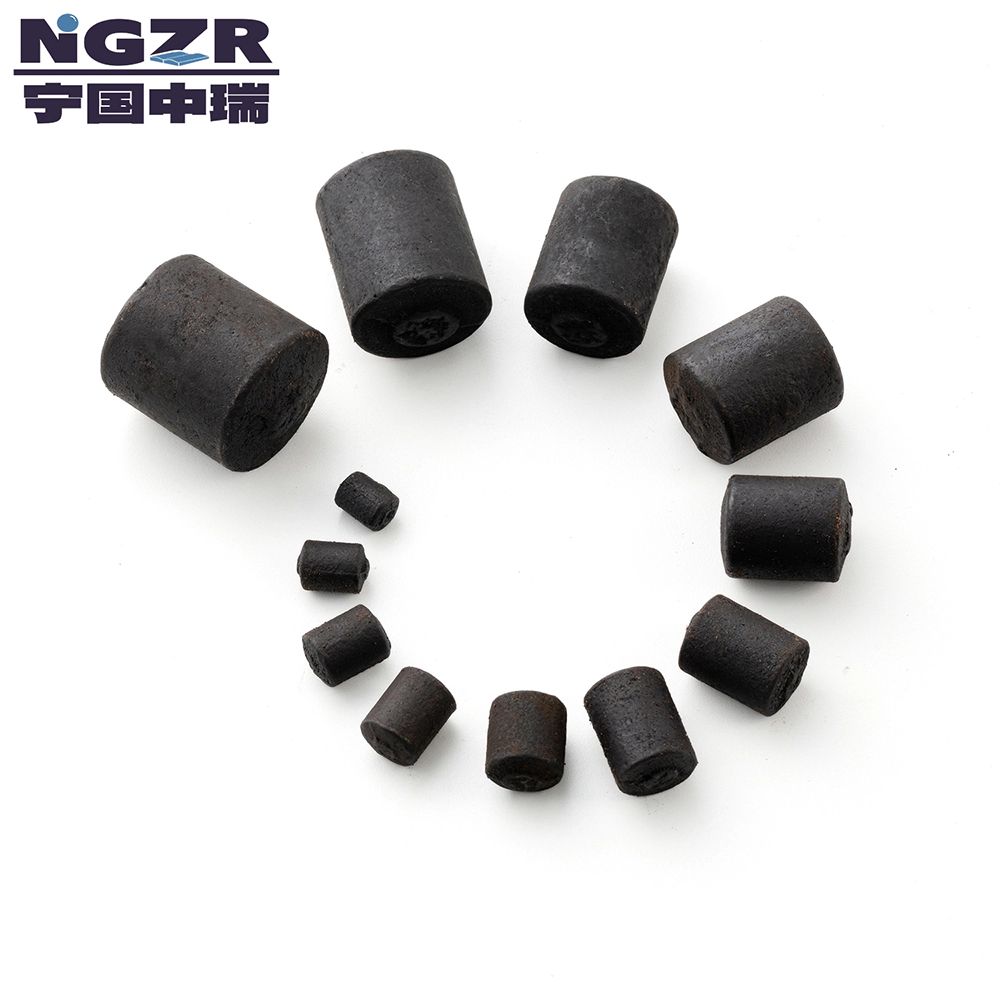
Casting Grinding Media is the consumable side of comminution — grinding balls, cylpebs, rods and cast sections in graded high-chromium cast iron, medium- and low-chromium alloys, CADI and forged media. Media from 6 mm to 40 mm suits fine and tower mill duty, while 40 mm to 150 mm serves ball mills and SAG mills in mining, cement and coal-fired power grinding.
Casting Mill Liner
Casting Mill Liner protects shells, end covers and grinding chambers: ball mill liners, SAG mill liners, vertical mill liners and rubber/Mn-Cr composite liners cast from high-chromium cast iron, high manganese steel and medium-chromium alloy steel. Liners are formed by lost foam precision casting and heat treated to stabilise the internal metallographic structure across the plate profile.
Casting Wear Parts for Mining Equipment
Spiral classifier wear parts and blades, excavator bucket adapters and bucket teeth sit in the material handling and classification stage, where abrasion from slurry, ore and overburden is continuous. Alloy steel and high manganese castings hold the profile that keeps classifier and bucket geometry working.
Steel Casting Parts
Beyond wear components, our steel casting capability covers functional parts such as brackets for solar photovoltaic mounting, steel caps for porcelain high-voltage insulators, and ductile iron pump and electric motor casings, cast in carbon steel, alloy steel, high manganese steel and wear-resistant alloy steel.
Product Range at a Glance
| Product family | Typical cast components | Material options | Application fit | Configuration data |
|---|---|---|---|---|
| Crusher wear casting parts | Hammers, blow bars, jaw plates, cheek plates, mantle and bowl liner, shredder knife hammers | High-chromium cast iron, bimetallic composite, high manganese steel, Mn-Cr alloy | Primary and secondary crushing, impact crushing, metal shredding and recycling | Crusher model, feed opening, feed size, closed-side setting, liner profile, bolt pattern |
| Casting grinding media | Grinding balls, cylpebs, cast sections, grinding rods, forged media | High-chromium, medium-chromium, low-chromium alloy; CADI; forged steel | Ball mills, SAG mills, tower mills, coal mills in cement, mining and power plants | Mill type and dimensions, ball diameter, charge weight, ore or clinker hardness, target wear life |
| Casting mill liner | Ball mill liners, SAG mill liners, vertical mill liners, composite liners | High-chromium cast iron, high manganese steel, medium-chromium alloy steel, Mn13Cr2, rubber-composite | Shell and end cover protection in horizontal ball mills, SAG mills and vertical mills | Mill diameter and length, chamber layout, plate thickness and profile, bolt hole pattern, radius |
| Wear parts for mining equipment | Classifier wear parts and blades, bucket adapters, bucket teeth | Wear-resistant alloy steel, high manganese steel | Spiral classifiers, mineral processing plants, excavators and loaders | Machine model, fitment interface, tooth and adapter profile, material handled |
| Steel casting parts | Solar photovoltaic brackets, steel caps for porcelain insulators, pump and motor casings | Carbon steel, alloy steel, high manganese steel, wear-resistant alloy steel, ductile iron | Energy and electrical infrastructure, pumps, general heavy machinery structures | Drawing and grade, dimensional tolerance, machining allowance, service environment |
Matching Alloy to Abrasion and Impact
Two wear mechanisms decide most casting specifications: low-stress scratching from fine, hard material, and high-stress impact from coarse feed or tramp metal. The alloy family is chosen against that balance rather than against a generic hardness target.
- High-chromium cast iron — abrasion-dominant duty in fine crushing, mill liners and grinding media.
- Medium- and low-chromium alloys — bulk media applications where wear cost per ton of ground product drives the choice.
- High manganese steel — work-hardening under impact, suited to jaw plates, hammers, bucket teeth and adapters.
- Bimetallic composite casting — a wear-resistant working layer on a tough backing for hammers and blow bars.
- Mn-Cr alloy and Mn13Cr2 — liner and jaw applications that need toughness and abrasion resistance together.
- CADI and forged media — SAG mill and high-impact milling where breakage resistance governs.
Wear life is set by the circuit as much as by the grade: ore competence, feed size distribution, mill speed, ball charge and water chemistry all move the wear curve. We therefore treat the material grade and the heat treatment cycle as one specification, confirmed against the actual duty rather than a catalogue default.
Critical Specifications, Capacity and Repeatability
- Media size range — Ф8 mm to Ф150 mm, with small cast balls and cylpebs from roughly 6 mm to 40 mm and large cast balls from 40 mm to 150 mm.
- Casting envelope — up to 5000 × 5000 × 1000 mm at up to 1,500 kg, and up to 1500 × 1500 × 1200 mm at up to 3,000 kg.
- Liner geometry — plate thickness, lifter profile, shell radius, hole pitch, bolt diameter and countersink depth held to the drawing.
- Crusher wear geometry — tooth and groove profile, cheek plate outline, mantle and bowl liner mating faces, blow bar mounting faces.
- Chemical composition — verified per heat before pouring by spectrometer and carbon-sulfur analysis.
- Hardness and structure — checked after heat treatment on the hardness tester and in the physical property testing room.
- Surface acceptance — smooth as-cast surface, free of cracks, slag inclusions, pores, sand holes, shrinkage cavities and cold shuts.
Process Control from Melt to Finished Casting
- IGBT module series-connected electric furnaces melt the charge under temperature control.
- A German-imported direct-reading spectrometer checks more than a dozen chemical elements within about one minute; pre-melt and post-melt analyses are run on every batch, and composition is corrected before pouring if it deviates.
- Molten steel temperature is measured by far-infrared instrument, and the automatic iron mould sand coating line performs constant-temperature pouring.
- Initial visual inspection rejects any part with surface cracks, slag inclusions, pores, sand holes, shrinkage cavities or cold shuts; accepted semi-finished castings are polished.
- Automatic temperature-controlled quenching with re-tempering, plus flipping annealing furnaces, sets the final hardness and toughness balance.
- Final hardness and property checks close the batch record before the finished product workshop releases the order.
Our management system is certified to ISO 9001 quality, ISO 14001 environmental and ISO 45001 occupational health and safety standards, with Safety Production Standardization certification and registered utility model patents covering production technology.
Installation, Fit and Maintenance Interface
Downtime is usually decided at installation rather than at casting. Liner segments are supplied to match the shell radius and bolt pattern, so hole pitch, countersink depth and plate-to-plate joint gaps are confirmed against the mill drawing before the shutdown window opens. Crusher wear parts are checked against the seating faces and wedge or bolt clamping arrangement of the specific machine.
Handling is part of the specification: heavy castings require defined lifting provisions and site rigging that matches unit weight. Once in service, liner wear is monitored by plate thickness at fixed reference points, and grinding media is replenished by size class so that the ball charge curve, not just the total tonnage, stays inside the design window. Keeping a matched spare set of liners, hammers or jaw plates on site shortens change-out time when wear reaches the replacement limit.
Information We Use to Configure Your Solution
We are mainly a manufacturer focused on customisation and can make products according to customer requirements. A quotation that holds up in production is built from the following inputs:
- Equipment make and model — crusher, mill, classifier, excavator or pump, including chamber or shell dimensions.
- Drawings, part numbers or a physical sample for existing wear parts, plus the mating face or bolt pattern.
- Material grade, hardness target or the current part's service life for comparison.
- Process data — feed size, throughput, mill speed, ball charge, ore or clinker type, moisture and working temperature.
- Required quantity, order pattern and any seasonal shutdown dates that affect the delivery plan.
- Machining or tolerance requirements on mating surfaces and mounting holes.
- Destination, packing preference and documentation requirements for the shipment.
Enquiries received on working days are answered within 12 hours, and technical points on geometry, alloy choice and heat treatment are settled before the pattern or mould is released to production.
Customer Questions
What wear-resistant castings does Zhongrui manufacture?
We cast high-chromium, medium-chromium and low-chromium alloy balls and cast sections, grinding cylpebs and rods, ball mill, SAG mill and vertical mill liners, crusher hammers, blow bars, jaw plates, cheek plates, cone mantle and bowl liners, shredder knife hammers, classifier wear parts, bucket teeth and adapters, plus structural steel castings such as solar photovoltaic brackets, insulator steel caps and ductile iron pump casings.
What size range and maximum casting weight can you supply?
Grinding media runs from Ф8 mm to Ф150 mm, with small balls and cylpebs in the 6 mm to 40 mm band and large cast balls from 40 mm to 150 mm. Individual castings are produced up to 5000 × 5000 × 1000 mm at up to 1,500 kg, or up to 1500 × 1500 × 1200 mm at up to 3,000 kg, using the moulding route that suits the part.
How do you choose between high-chromium cast iron and high manganese steel?
The decision follows the dominant wear mechanism at the working point. High-chromium cast iron performs where fine, hard material produces scratching abrasion; high manganese steel is used where coarse feed or tramp metal generates impact and the surface work-hardens in service. Where both occur, bimetallic composite casting or an Mn-Cr alloy provides the compromise.
How is quality controlled before an order is released?
Composition is analysed before and after melting on a cabinet-type PRO spectrometer, supported by a carbon-sulfur analyzer, and corrected before pouring. Pouring temperature is monitored by far-infrared instrument on the constant-temperature line. After heat treatment, hardness and physical properties are checked, and every casting passes a visual inspection for cracks, porosity, sand holes, shrinkage cavities and cold shuts. Our operations run under ISO 9001, ISO 14001 and ISO 45001 certification.
What do you need from us to prepare a proposal?
Send the equipment model and chamber or shell dimensions, a drawing, part number or sample of the current wear part, the material grade or expected life, and the process conditions — feed size, throughput, mill speed, charge and material type. Quantity, required delivery timing, machining requirements and destination complete the picture, and we return a configuration and quotation that states the alloy, heat treatment and geometry we propose.



