


 English
 русский
Casting Bucket Adapters Cast for Mining and Heavy Loading
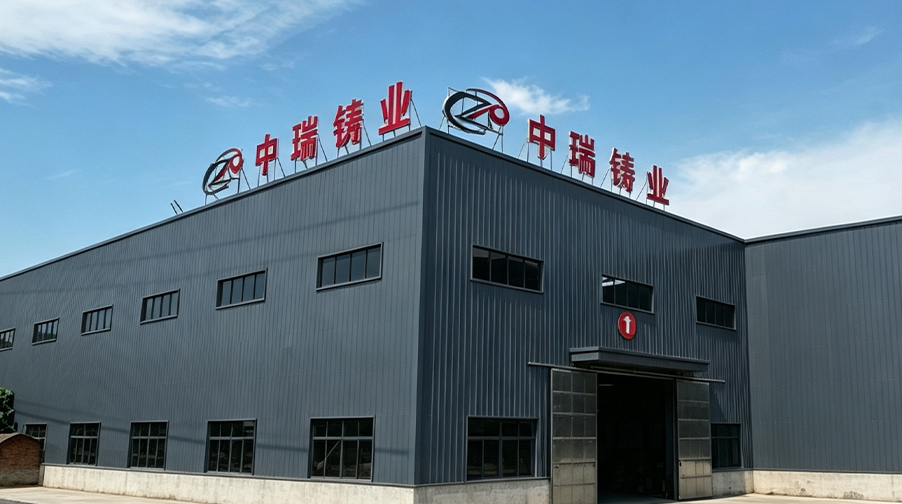
Anhui Ningguo Zhongrui Wear-Resistant Materials Co., Ltd. casts bucket adapters, bucket teeth and heavy-duty wear castings for hydraulic excavators, wheel loaders and mining shovels. We are a Casting Bucket Adapter manufacturer working from Ningguo City, Anhui Province, China, pouring high-manganese steel, chromium alloy steel and high-chromium iron in our own foundry, then heat treating, hardness testing and visually inspecting each batch before packing.
Adapters leave our works as individual castings, as adapter-and-tooth assemblies, or as a complete bucket GET package matched to the machine, the lip and the material being dug. Because the same foundry also casts the tooth, the liner and the crusher wear part that follow the adapter in the production line, nose geometry and tooth fit stay consistent across repeat orders.
Our mining wear range
- Casting Bucket Adapter — weld-on and pin-on noses for excavator, loader and shovel buckets, cast to a customer tooth system or to a supplied worn sample.
- Casting Bucket Tooth — matching teeth in chisel, blunt and heavy-duty profiles for the same adapter interface.
- Casting Classifier Wear Parts — spiral classifier blades and related mineral-processing wear castings.
- Casting Wear Parts for Mining Equipment — hammers, jaw plates, cone liners and other crushing consumables.
- Grinding media, mill liners and Steel Casting Parts for the surrounding plant equipment.
Adapter Configurations We Cast
Adapter selection begins with the tooth system and the bucket lip, not with the casting weight. The configurations below cover most mining, quarry and rehandling duties, and each one can be poured in the grade that matches its dominant wear mechanism.
| Adapter configuration | Interface | Typical base grade | Application fit |
|---|---|---|---|
| Weld-on top-leg nose | Pin-on tooth, vertical or horizontal pin | High manganese steel | Excavator and loader buckets in shot rock and ore |
| Bolt-on adapter | Bolted lip plate, replaceable without cutting | Quenched and tempered alloy steel | Mobile fleets where field welding is impractical |
| Long-nose pin-on adapter | OEM tooth series with pin and retainer | Alloy steel or high manganese | Primary digging in abrasive overburden and ore |
| Chisel-point nose | Narrow nose for penetration | Heat-treated alloy steel | Compacted ground, clay and hard stratified rock |
| Blunt wide nose | Wide nose for wear life | High-chromium or alloy steel | Rehandling sand, gravel, slag and sinter |
| Corner and side-cutter adapter | Bucket corner or wing position | High manganese steel | Protection of bucket corners and side plates |
| Custom pattern adapter | Customer drawing or worn sample | Selected to duty | Legacy machines and non-standard bucket lips |
Fitment interfaces we work to
- Standard digging tooth series and their pin, washer and retainer sets, including left- and right-hand configurations.
- Pin hole diameters, pin centres, retainer seats and nose angles measured from the customer's sample or taken from the drawing.
- Bucket lip thickness, lip angle and bevel details for weld-on noses, so the adapter sits flush on the plate before welding.
- Machine class and bucket capacity, used to check that the nose section is proportionate to the digging force applied.
Material Selection for Adapter Bodies and Noses
Impact and abrasion rarely appear in the same proportion on one bucket. High manganese steel work-hardens under repeated shock and resists cracking where broken rock strikes the nose; quenched and tempered chromium alloy steel holds a higher initial hardness where sliding abrasion dominates and impact is moderate. We confirm the grade, the hardness range and the heat treatment cycle in the quotation rather than leaving the material open.
- High manganese steel — the default where shock loading from oversize rock is the controlling failure mode.
- Chromium alloy steel, quenched and tempered — for abrasive ore and rehandling duties with a stable, higher as-cast hardness.
- High-chromium iron and bimetallic composite — used in our wear-part programme for high-abrasion, low-impact positions such as liners and classifier blades.
- Hardness is verified on the finished casting with our bench hardness tester, and chemistry is checked with the cabinet-type PRO spectrometer and carbon-sulfur analyzer before pouring.
Critical Specifications Confirmed Before Pouring
Every adapter order is fixed against a short list of dimensional and metallurgical data. These values drive the pattern, the riser and gating design, the machining allowance and the final inspection record.
- Nose height and width, top and bottom leg thickness, throat opening and overall length.
- Pin hole diameter, pin centre distance, retainer pocket depth and retention method.
- Weld bevel geometry, contact face flatness and the fit-up gap allowed on the lip.
- Casting weight per piece, machining allowance on wear faces, and marking of heat number and part reference.
- Hardness range, microstructure requirement and the sampling position for destructive testing, where specified.
Casting, Heat Treatment and Batch Control
Adapter bodies are poured on the same lines that supply our crusher and mill wear programme, so process control is shared rather than improvised. Melting is temperature controlled in VIP-1800 series furnaces, pouring temperature is measured with a far-infrared thermometer, and heat treatment runs on an automatic quenching plus reheat line with two automatic flipping annealing furnaces.
| Plant asset | What it contributes |
|---|---|
| Fully automatic lost foam precision casting line | Near-net-shape adapters and complex wear castings with reduced machining allowance |
| 2 automatic iron mould sand-coating lines, 4 robotic arm shell moulding machines | Repeatable mould filling and wall thickness across repetitive wear-part batches |
| Resin-sand moulding with wooden patterns | Large-section castings up to 5000 × 5000 × 1000 mm and single-piece weights up to 3000 kg |
| 3 × VIP-1800 melting furnaces | Temperature-controlled melting and consistent pouring temperature between batches |
| Automatic quenching and reheat line, 2 annealing furnaces | Hardness and toughness control with repeatable thermal cycles |
| PRO spectrometer, carbon-sulfur analyzer, hardness tester | Chemistry and hardness records issued with the casting batch |
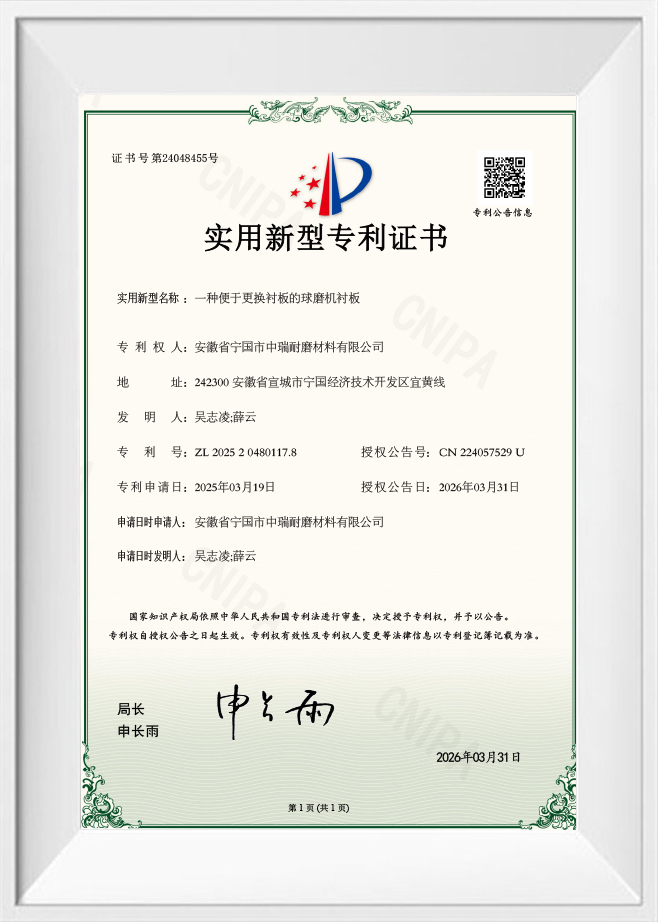
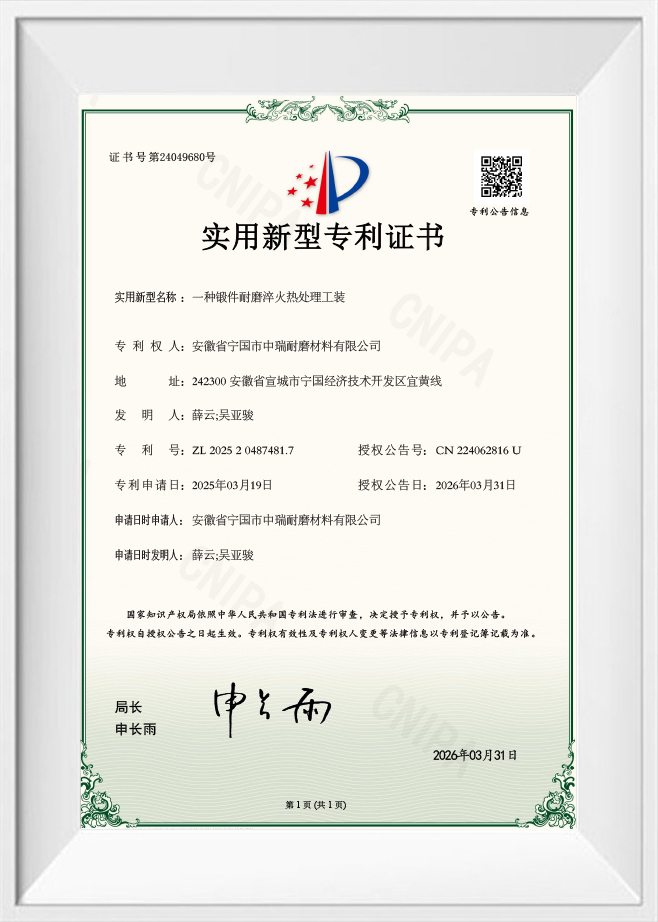
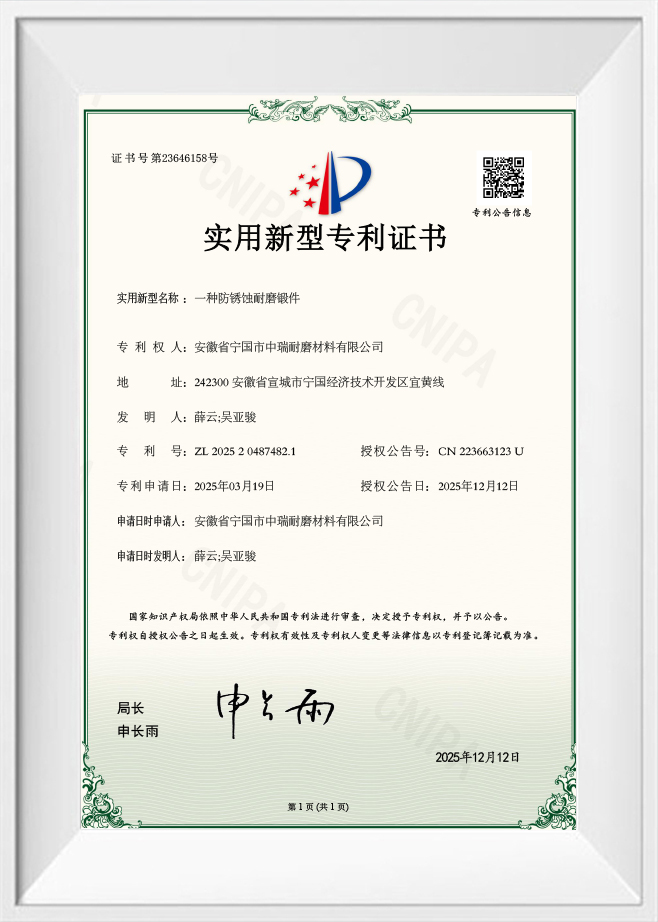
Castings pass a visual inspection for surface cracks, slag inclusions, gas pores, sand holes, shrinkage cavities and cold shuts before finishing, and semi-finished parts are cleaned and dressed afterwards. Our management system is certified to ISO9001, ISO14001 and ISO45001, we hold safety production standardisation certification, and utility model patent certificates cover several casting and heat-treatment arrangements developed in-house. Annual capacity for cast balls and castings stands at 60,000 tonnes.
Configuration Options and Custom Work
Most adapter enquiries are settled by four choices: fastening method, nose profile, material grade and retention style. We then handle the pattern, the sample-based reverse drawing and the marking that the customer's maintenance system needs.
- Weld-on, bolt-on or pin-on attachment, with left-hand and right-hand variants held as separate patterns.
- Chisel, blunt, heavy-duty or long-nose profiles within the same bucket series.
- Pin, washer and retainer seats cast to suit the tooth the customer already stocks.
- Part reference, heat number and customer logo cast or stamped for traceability on site.
- Repeat-order patterns retained so that a later batch matches the original nose geometry.
Installation, Maintenance and Spare Parts
Weld-on adapters are positioned with the bevel seated against the lip, tacked on both sides and then welded with a consumable matched to the adapter grade and the bucket steel. Heat input and interpass temperature are controlled, and the weld sequence alternates along the joint to limit distortion before the tooth and retainer are fitted.
- Fit-up and finish checks before welding: nose squareness to the lip, pin hole alignment and free seating of the tooth.
- Wear measurement at the nose at fixed service intervals, with replacement planned against tonnes moved rather than calendar time.
- Pin, washer and retainer supplied as spares, together with matching teeth, so a bucket can be kept in service between adapter changes.
- Casting heat numbers recorded on the packing list, allowing a later reorder to be traced back to the same pattern and thermal batch.
Information We Use to Configure Your Solution
A quotation is prepared from the machine, the interface and the duty. The clearer the input, the fewer assumptions sit behind the drawing and the price.
| Input we need | How we use it |
|---|---|
| Machine make, model and bucket capacity | Sizing the nose section against real digging force |
| Tooth system, pin diameter and retention style | Fixing pin centres, retainer pocket and nose angle |
| Drawing, worn sample or measured sketches | Confirming geometry and setting the pattern shrinkage |
| Bucket lip thickness and weld-on position | Bevel design, contact face flatness and fit-up gap |
| Rock type, abrasiveness and impact level | Material grade and hardness range selection |
| Annual quantity, wear cycle and replacement plan | Batch size, pattern retention and spare-parts coverage |
| Packing, marking and documentation requirements | Shipping scope and the inspection record issued with the goods |
Frequently Asked Questions
Which bucket adapter configurations can you cast?
Weld-on top-leg noses, bolt-on adapters, long-nose pin-on adapters, chisel and blunt profiles, corner and side-cutter adapters, and fully custom patterns based on a drawing or a worn sample. Left-hand and right-hand versions are held as separate patterns.
What materials do you use for adapter bodies?
High manganese steel where breaking rock gives the highest shock load, and quenched and tempered chromium alloy steel where sliding abrasion controls life. High-chromium iron and bimetallic composite castings are used in our programme for high-abrasion, low-impact wear parts.
What information should be sent with an adapter enquiry?
Machine make and model, tooth system, pin diameter and retainer style, a drawing or worn sample, bucket lip thickness for weld-on noses, the working material, and the expected annual quantity. A photograph of the bucket corner and lip also helps confirm fit-up.
How is quality verified on a bucket adapter batch?
Chemistry is checked with the PRO spectrometer and carbon-sulfur analyzer before pouring, hardness is measured on finished castings, and every part is visually inspected for cracks, pores, slag inclusions, shrinkage cavities and cold shuts before dressing and packing.
Can you supply adapters together with matching teeth and spares?
Yes. Adapters, teeth, pins, washers and retainers can be shipped as a matched set from the same foundry, which keeps the nose and tooth interface consistent when the bucket is rebuilt or when a second machine of the same class is added.
Do you keep patterns for repeat orders?
Patterns and sample measurements are retained against the customer part reference, and heat numbers are recorded on the packing list, so a repeat order reproduces the original geometry and thermal batch conditions.



